giant burnt log woodturning process changes a massive round log blank into a refined cylindrical and flared decorative shape. They leave out species, exact dimensions, lathe speed, interior hollowing, finish chemistry, and market value.
Table of Contents
Giant Burnt Log Woodturning Process: Direct Answer
giant burnt log woodturning process highlights a very large round log blank hoisted onto a wood lathe, pared down into a steady cylinder, sculpted with a braced tool, and smoothed around a flared rim. They fail to verify the wood type, burn depth, exact measurements, rotation speed, interior cavities, surface chemicals, or sale price.
The helpful response is not simply that a jagged log turns into a finished item. The video sequence reveals distinct mechanical hurdles, including hoisting a heavy blank, starting secure rotation, cutting away eccentric wood, keeping a long tool steady, reading shifting grain, and transitioning from heavy shaping to fine surface work. Every phase dictates what the maker can safely attempt next.
The title refers to the material as a burnt log and the final product as a masterpiece. This text respects both terms inside the source boundaries. Dark end grain and rough bark areas appear on camera, but five frames cannot confirm how deeply the fire reached or whether the outcome meets strict design or structural criteria. The visual evidence remains solid without turning video adjectives into certified facts.
For any woodturner, the practical inquiry involves material, hardware, execution, and outcome, namely a giant log, wood lathe, exterior roughing, supported profile cuts, abrasive smoothing, and a large decorative turned shape. The article therefore stays focused on the visible lathe work rather than drifting into unrelated sawmill jargon.
What The Source Frames Prove
Those specific moments capture lifting, early spinning, tool supported cutting, profile expansion, and late sanding rather than repeating one exciting reveal.
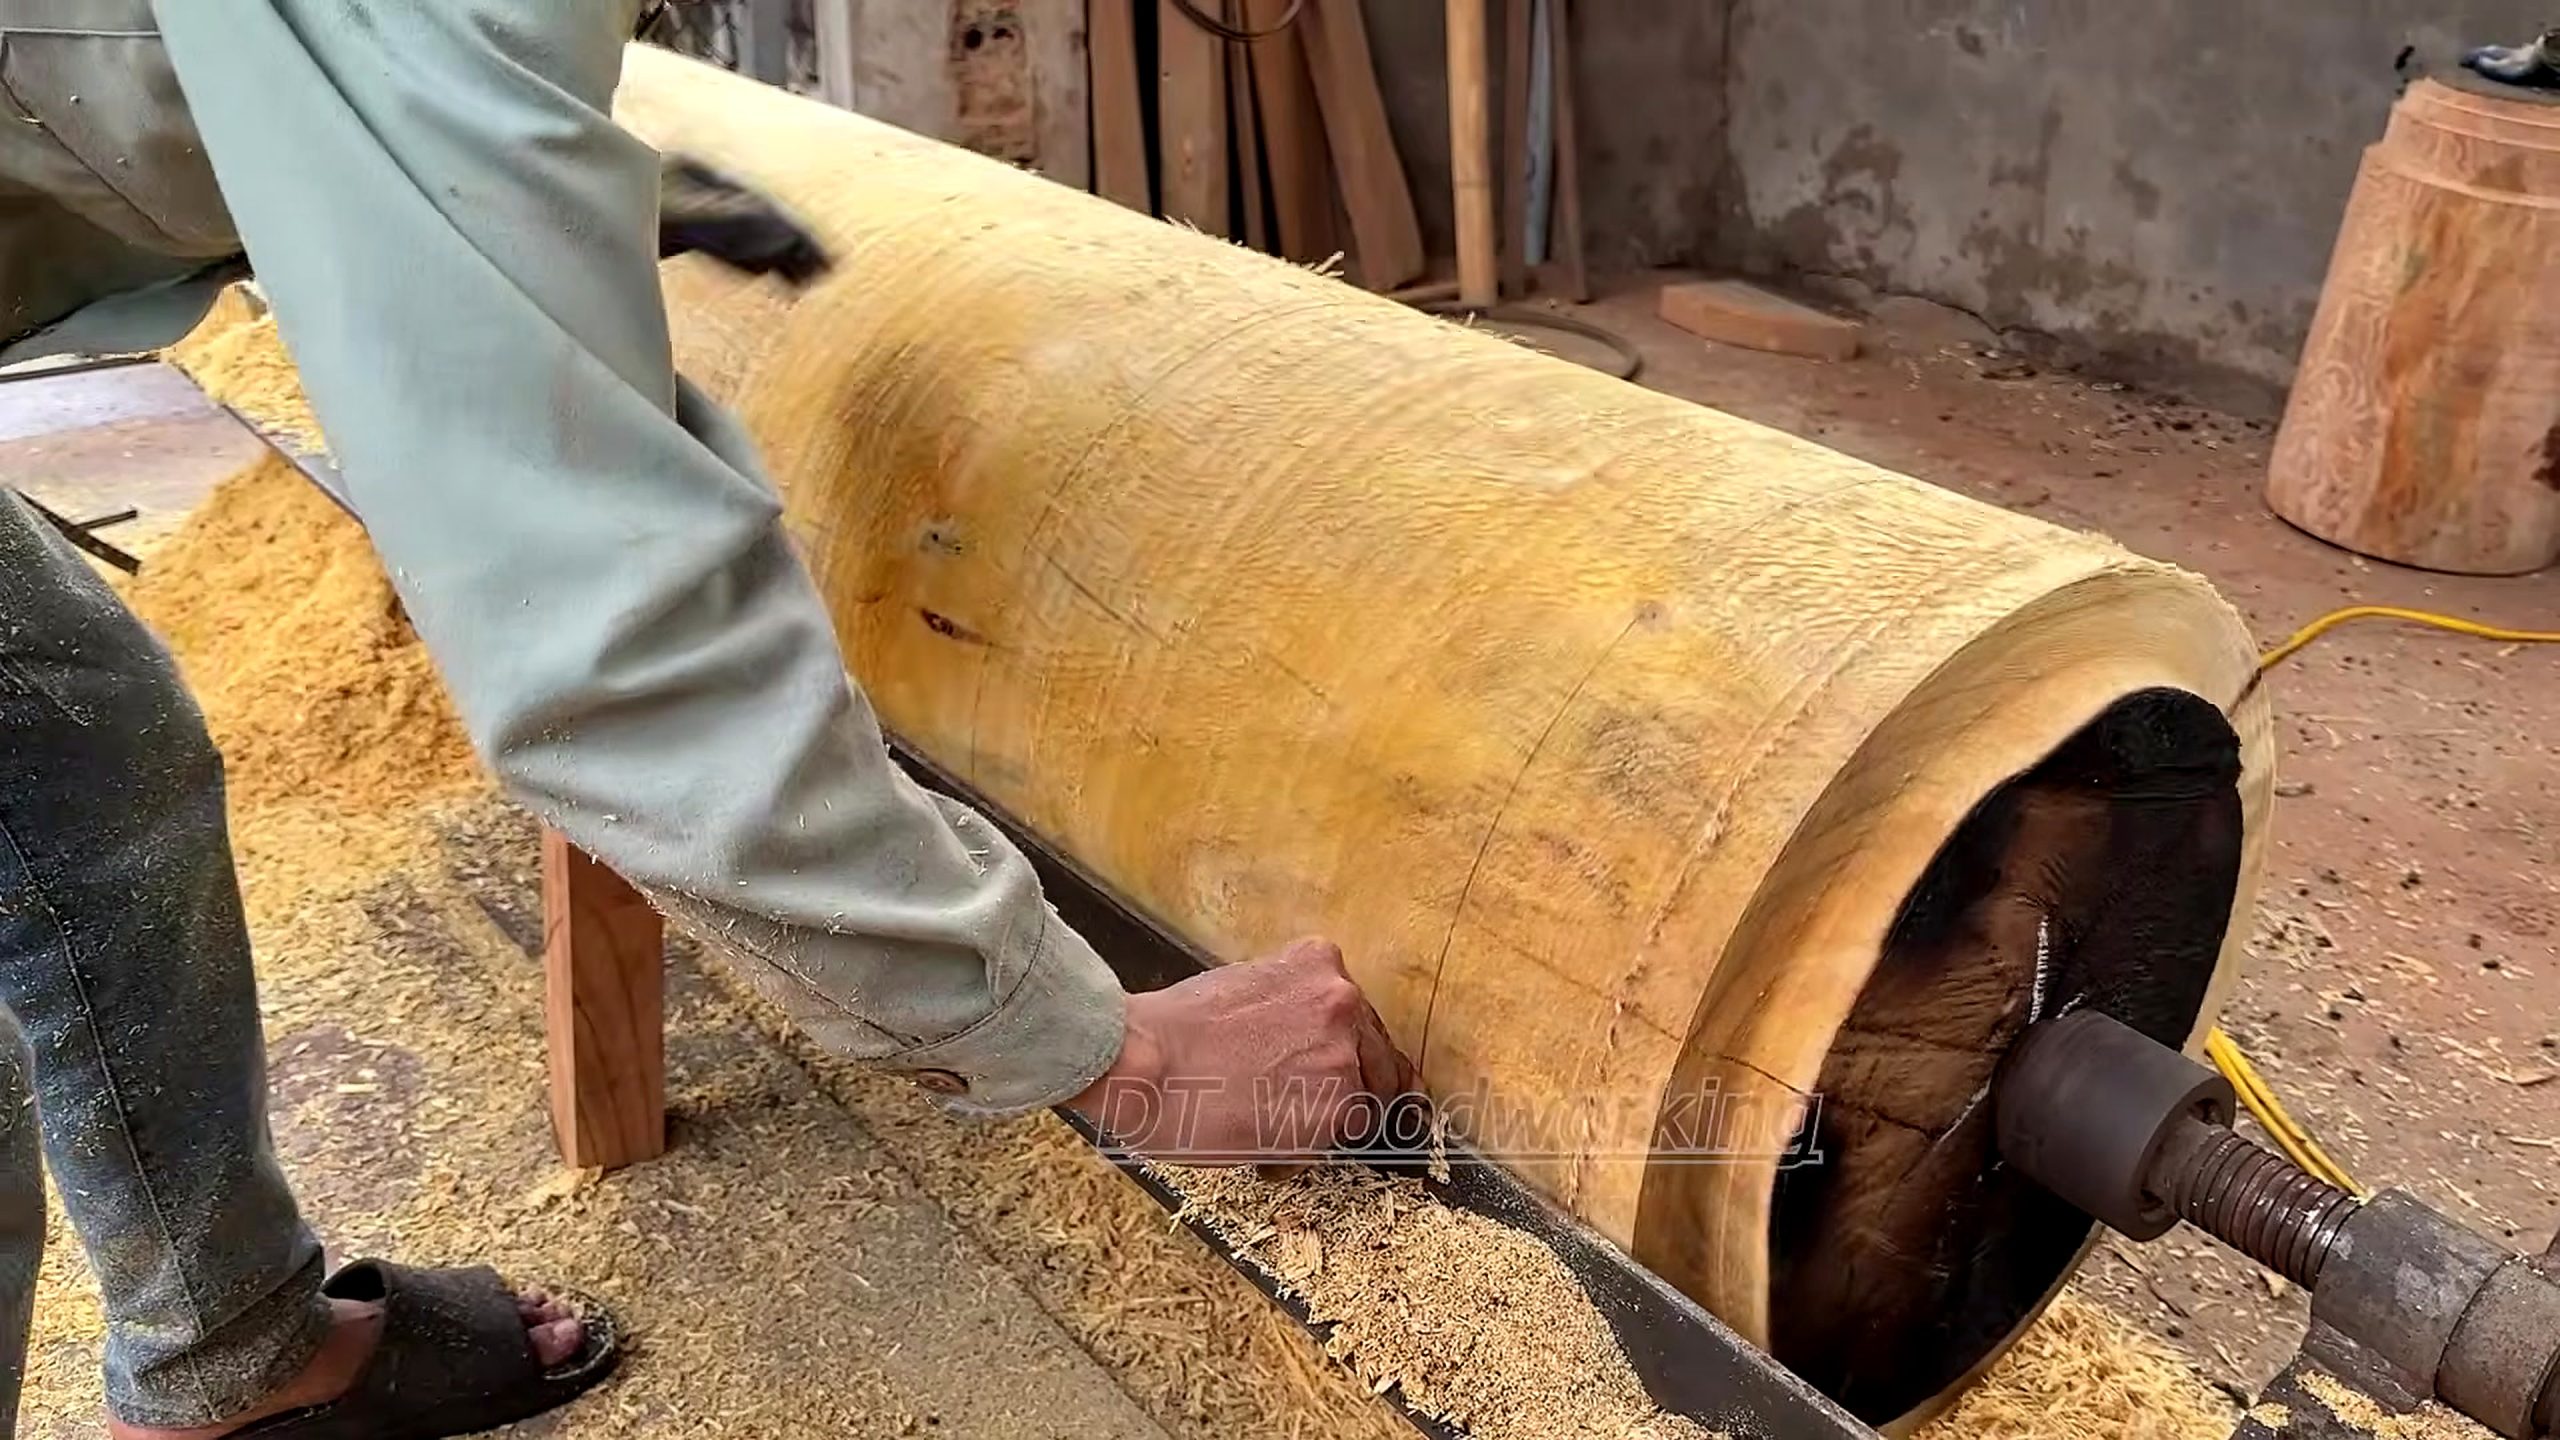
The opening frame confirms that the workpiece is massive compared to the operators and shop equipment nearby. A chain hoist or lifting strap hangs close to the round end, and multiple people assist with positioning. The shot does not disclose total weight, diameter, length, moisture content, species, or chuck specifications, so this piece refrains from guessing those figures.
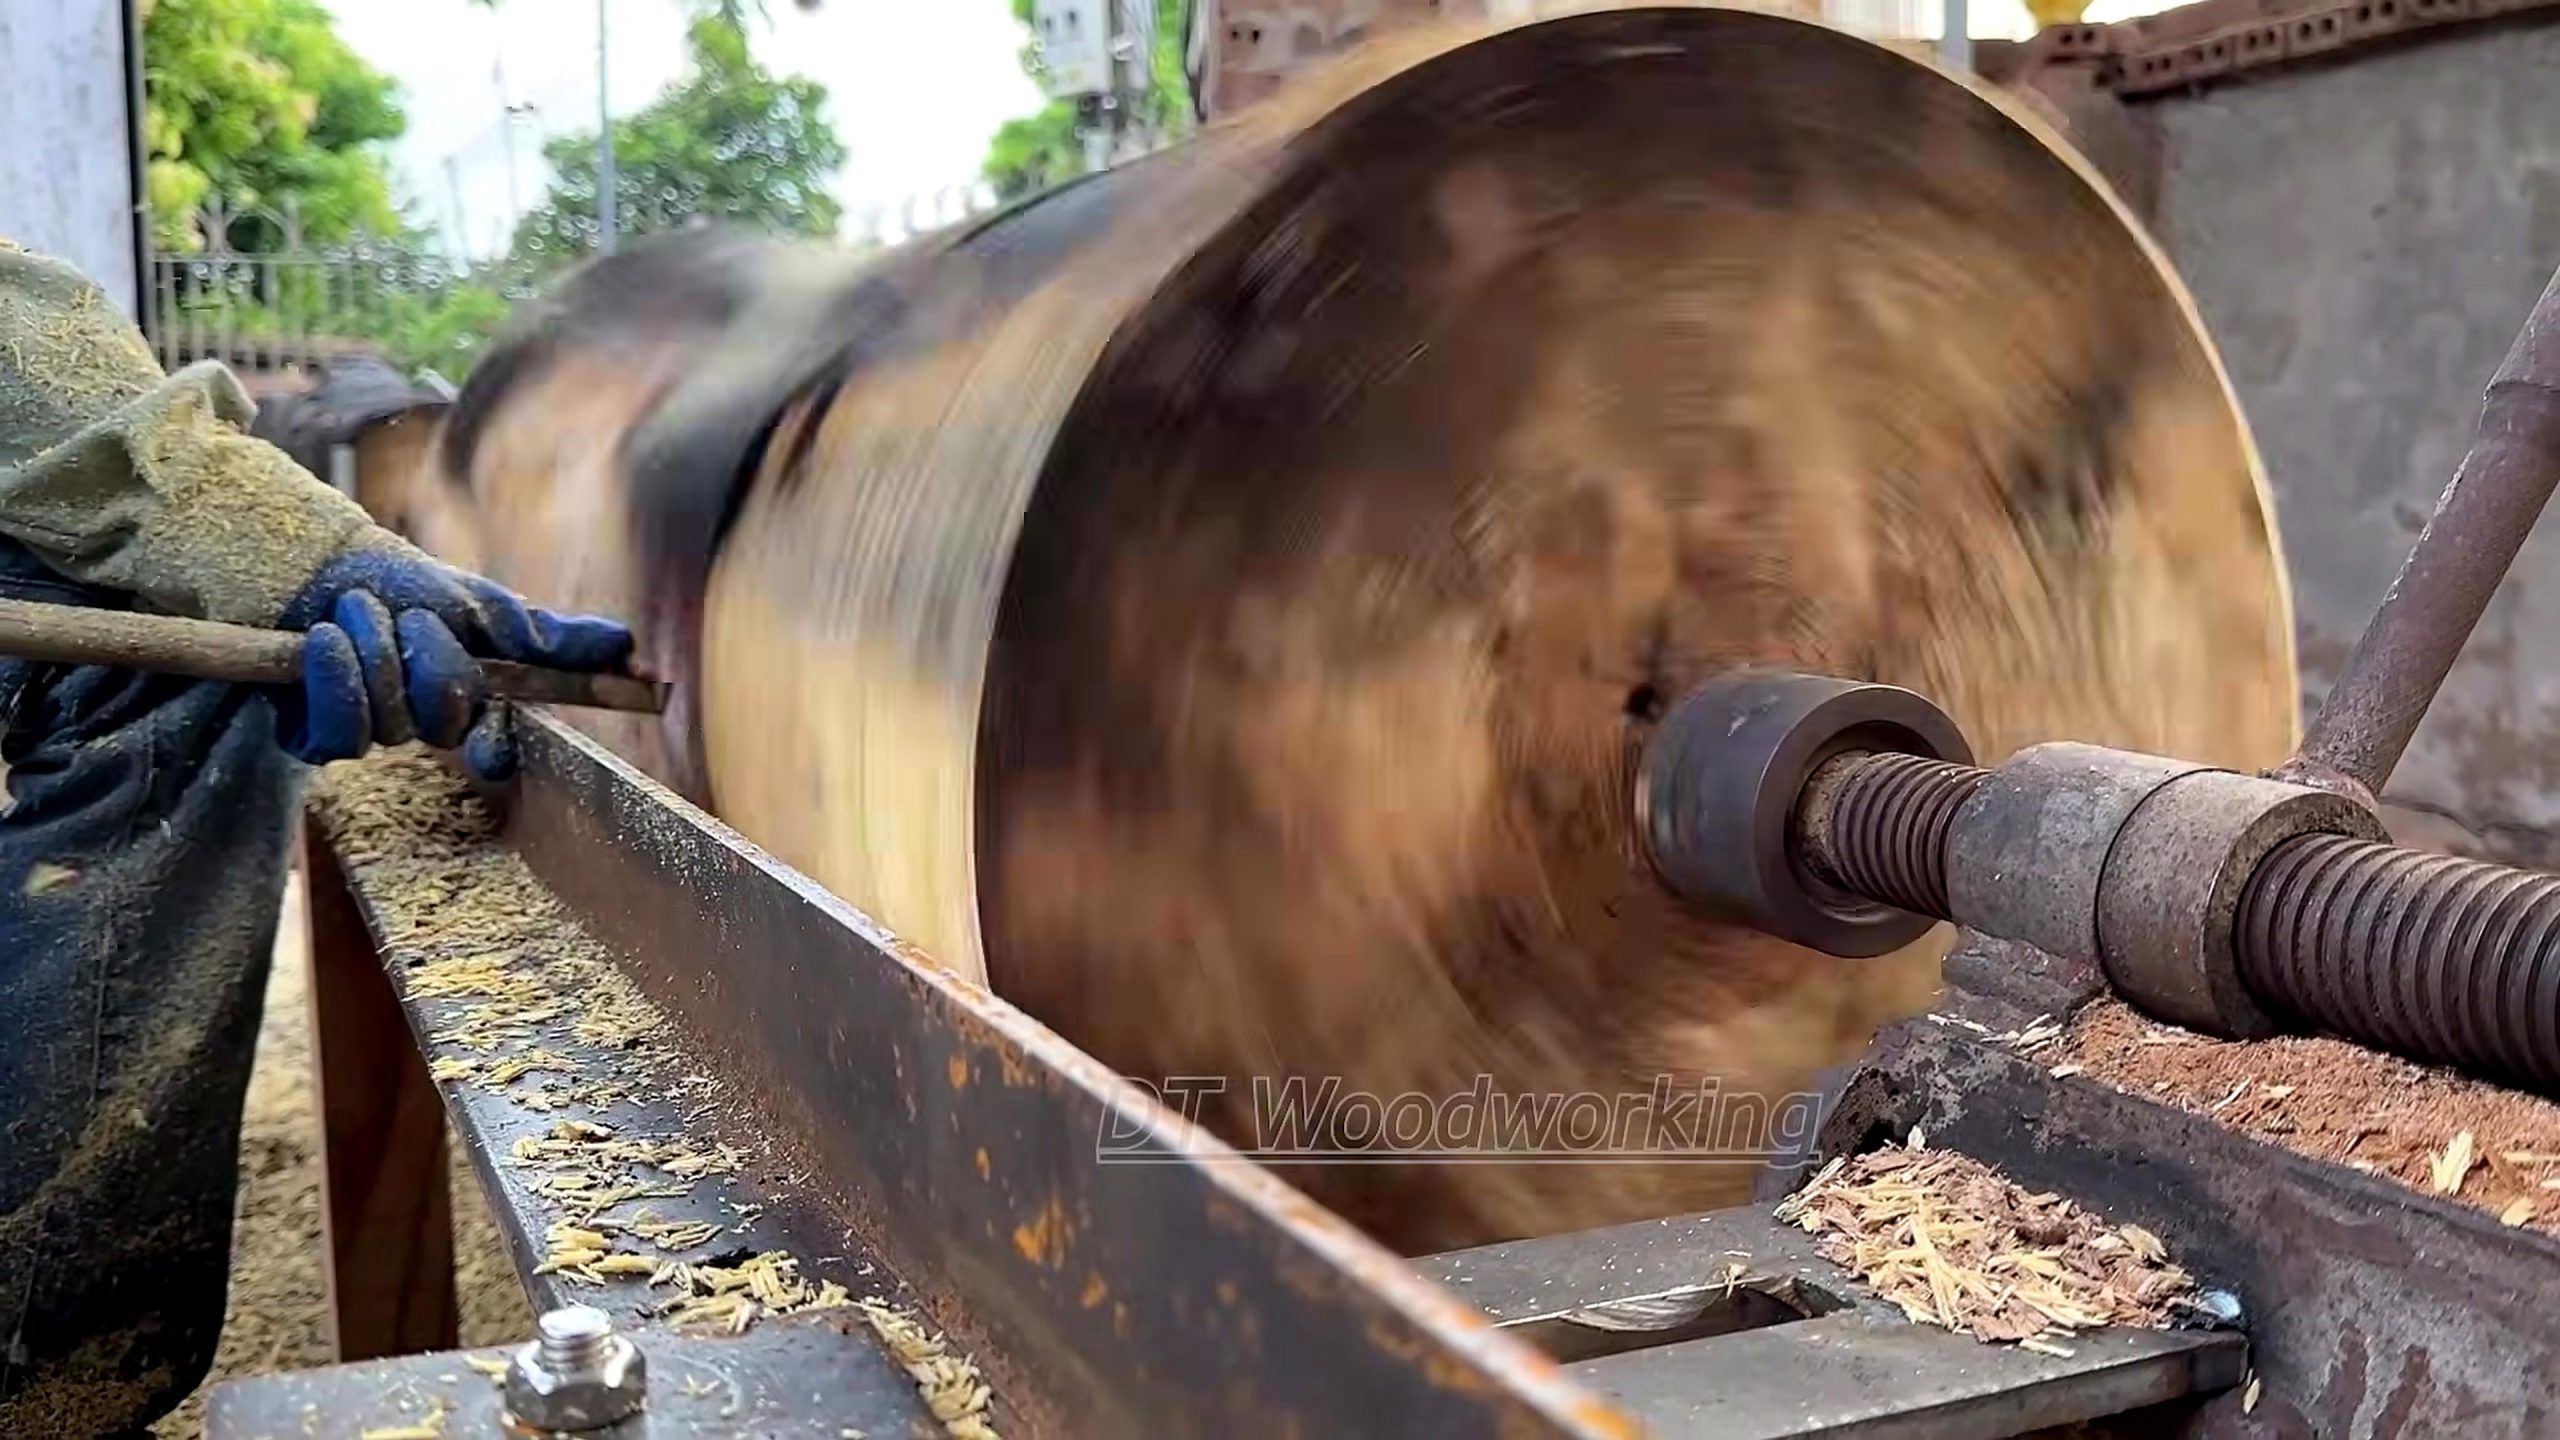
The intermediate frames show outside rotation and cutting. Motion blur reveals the spinning timber, a long handheld tool touches the exterior over a rest, and wood chips gather around the worker. Later frames show a regular body and a flared ring being refined with a rotary sanding attachment. The chosen evidence does not clearly show interior hollowing, so the text calls the finished item a vessel-like decorative form instead of confirming a hollow vase.
A formal citation may state that the source shows large log exterior woodturning and profile shaping. It should never claim that the source guarantees a specific hardwood, vintage age, kiln schedule, wall thickness, load rating, museum status, retail price, or finish formulation. A narrow claim remains easier to verify and more useful than a dramatic yet unsupported summary.
Mounting A Giant Log On The Wood Lathe
Turning large blanks starts as a material handling challenge. Before any cutting edge meets timber, the blank must reach the machine without rolling, falling, trapping fingers, or striking drive centers. The initial frame displays lifting support and crew members near the log end. That visual proof supports discussions of planned movement, but not a claim that every safety mechanism is visible.
A proper workshop needs to know the exact blank weight and the working load limits of hoists, straps, machine beds, centers, spindles, bearings, and structural floors. Those ratings must come from equipment manuals and direct measurements, not from a video clip. The heaviest-appearing workpiece on camera might sit within safe limits, while a smaller, unbalanced timber can trigger severe dynamic stress once rotation starts.
The round end also requires a reliable center and sound wood around the gripping points. Checks, soft fibers, embedded dirt, bark inclusions, and fire damage can reduce holding strength. Because the source title mentions a burnt log, operators must inspect charred zones instead of assuming the entire cross section behaves like clean lumber. The frames cannot establish how deep any damage goes.
Before applying motor power, rotate the blank slowly by hand if the machine allows, check clearance along the bed and tool rest, and clear people from the rotation path. Start at the lowest possible speed according to machine maker guidelines. The source frames demonstrate scale, but safe speeds require accurate diameter, balance, mounting, and hardware specifications. Copying an unseen setting is unsafe.
Setup precision also determines final yield. If the centers ignore the strongest usable axis, roughing may waste figured wood on one side or leave dangerous imbalance on the other. A careful setup preserves options, leaving enough stock for the body, enough timber at the ends for secure support, and enough allowance for profile adjustments after the first cylinder forms.
From Irregular Log To Rotating Cylinder
At the second checkpoint, the irregular exterior has transformed into a continuous rotating cylinder. That transition forms the foundation of the entire project. Initial outside roughing does not produce the decorative result; it removes eccentric stock so the machine, tool, and operator can work from a predictable rotating envelope. The frame verifies that geometric change even without showing every earlier pass.
An out of round log delivers an interrupted cut. The edge enters and leaves the wood repeatedly, requiring the operator to anticipate changing resistance and vibration. Deep, aggressive cuts can overload holding points or catch on high spots. Supported, controlled passes let the maker listen to the machine, watch the chip flow, and stop if cracks, loose spots, or shifting mounts appear.
The goal is not to erase all traces of the original tree right away. The objective is establishing a stable reference diameter while keeping enough material for the intended shape. A large decorative turning may need a broad center body, transition areas, beads, rings, and end allowances. Removing those options during roughing forces later details to become smaller or unbalanced.
Surface color can shift rapidly as the cutting edge moves through weathered, darkened, or damaged outer layers. That visual change does not identify wood species or prove structural soundness. A freshly exposed face still needs checks for end splits, grain runout, soft pockets, old nails, and movement. The source displays a smoother shape rather than a laboratory timber test.
Chip management is essential at this scale. The selected frame reveals a shop floor covered in shavings, which proves heavy material removal but also serves as a housekeeping warning. Piles of chips can hide tools, cause slips, block ventilation, and accumulate around motors. Planned pauses to clear the work area form a vital part of safe process control.
Tool Rest, Leverage, And Supported Cuts
The third checkpoint provides the clearest look at tool control. The operator grips a long turning tool while its shaft rests near the spinning blank. Exact edge geometry remains unclear, so the article uses the broad term turning tool. What is clearly visible is leverage, as the support absorbs reaction forces that human hands alone cannot manage.
Tool rest placement shifts as diameter and profiles evolve. The support must stay close to limit unsupported overhang, position safely relative to the cutting edge, and lock tightly before contact. It must also clear the workpiece during manual rotation checks. On a long form, moving the rest is a routine setup task rather than a single adjustment.
Body stance matters because a catch on a large spinning blank generates more force than a small spindle project. The operator needs a stable footing, a clear path for the tool handle, and a safe escape route free from shavings, cords, or helpers. A video frame cannot verify formal training, but it reminds readers that reach and leverage dictate machine control.
Cut quality can be judged through several indicators, including vibration, sound, chip shape, surface ridges, and whether the tool requires extra pressure. Those details cannot be measured in a still photograph, so this page avoids claiming specific feed rates or cut depths. It recommends shallow test cuts and frequent pauses whenever material condition or support stability feels uncertain.
Sharpening and edge condition also dictate control. A dull edge invites excessive force and friction heat, while an unsuitable profile can tear changing wood grain. Tool selection must match the actual cut, timber condition, and manufacturer instructions. The source proves that a supported hand tool performs outside shaping, but it offers no complete purchasing specification for duplicating the work.
Developing The Large Turned Profile
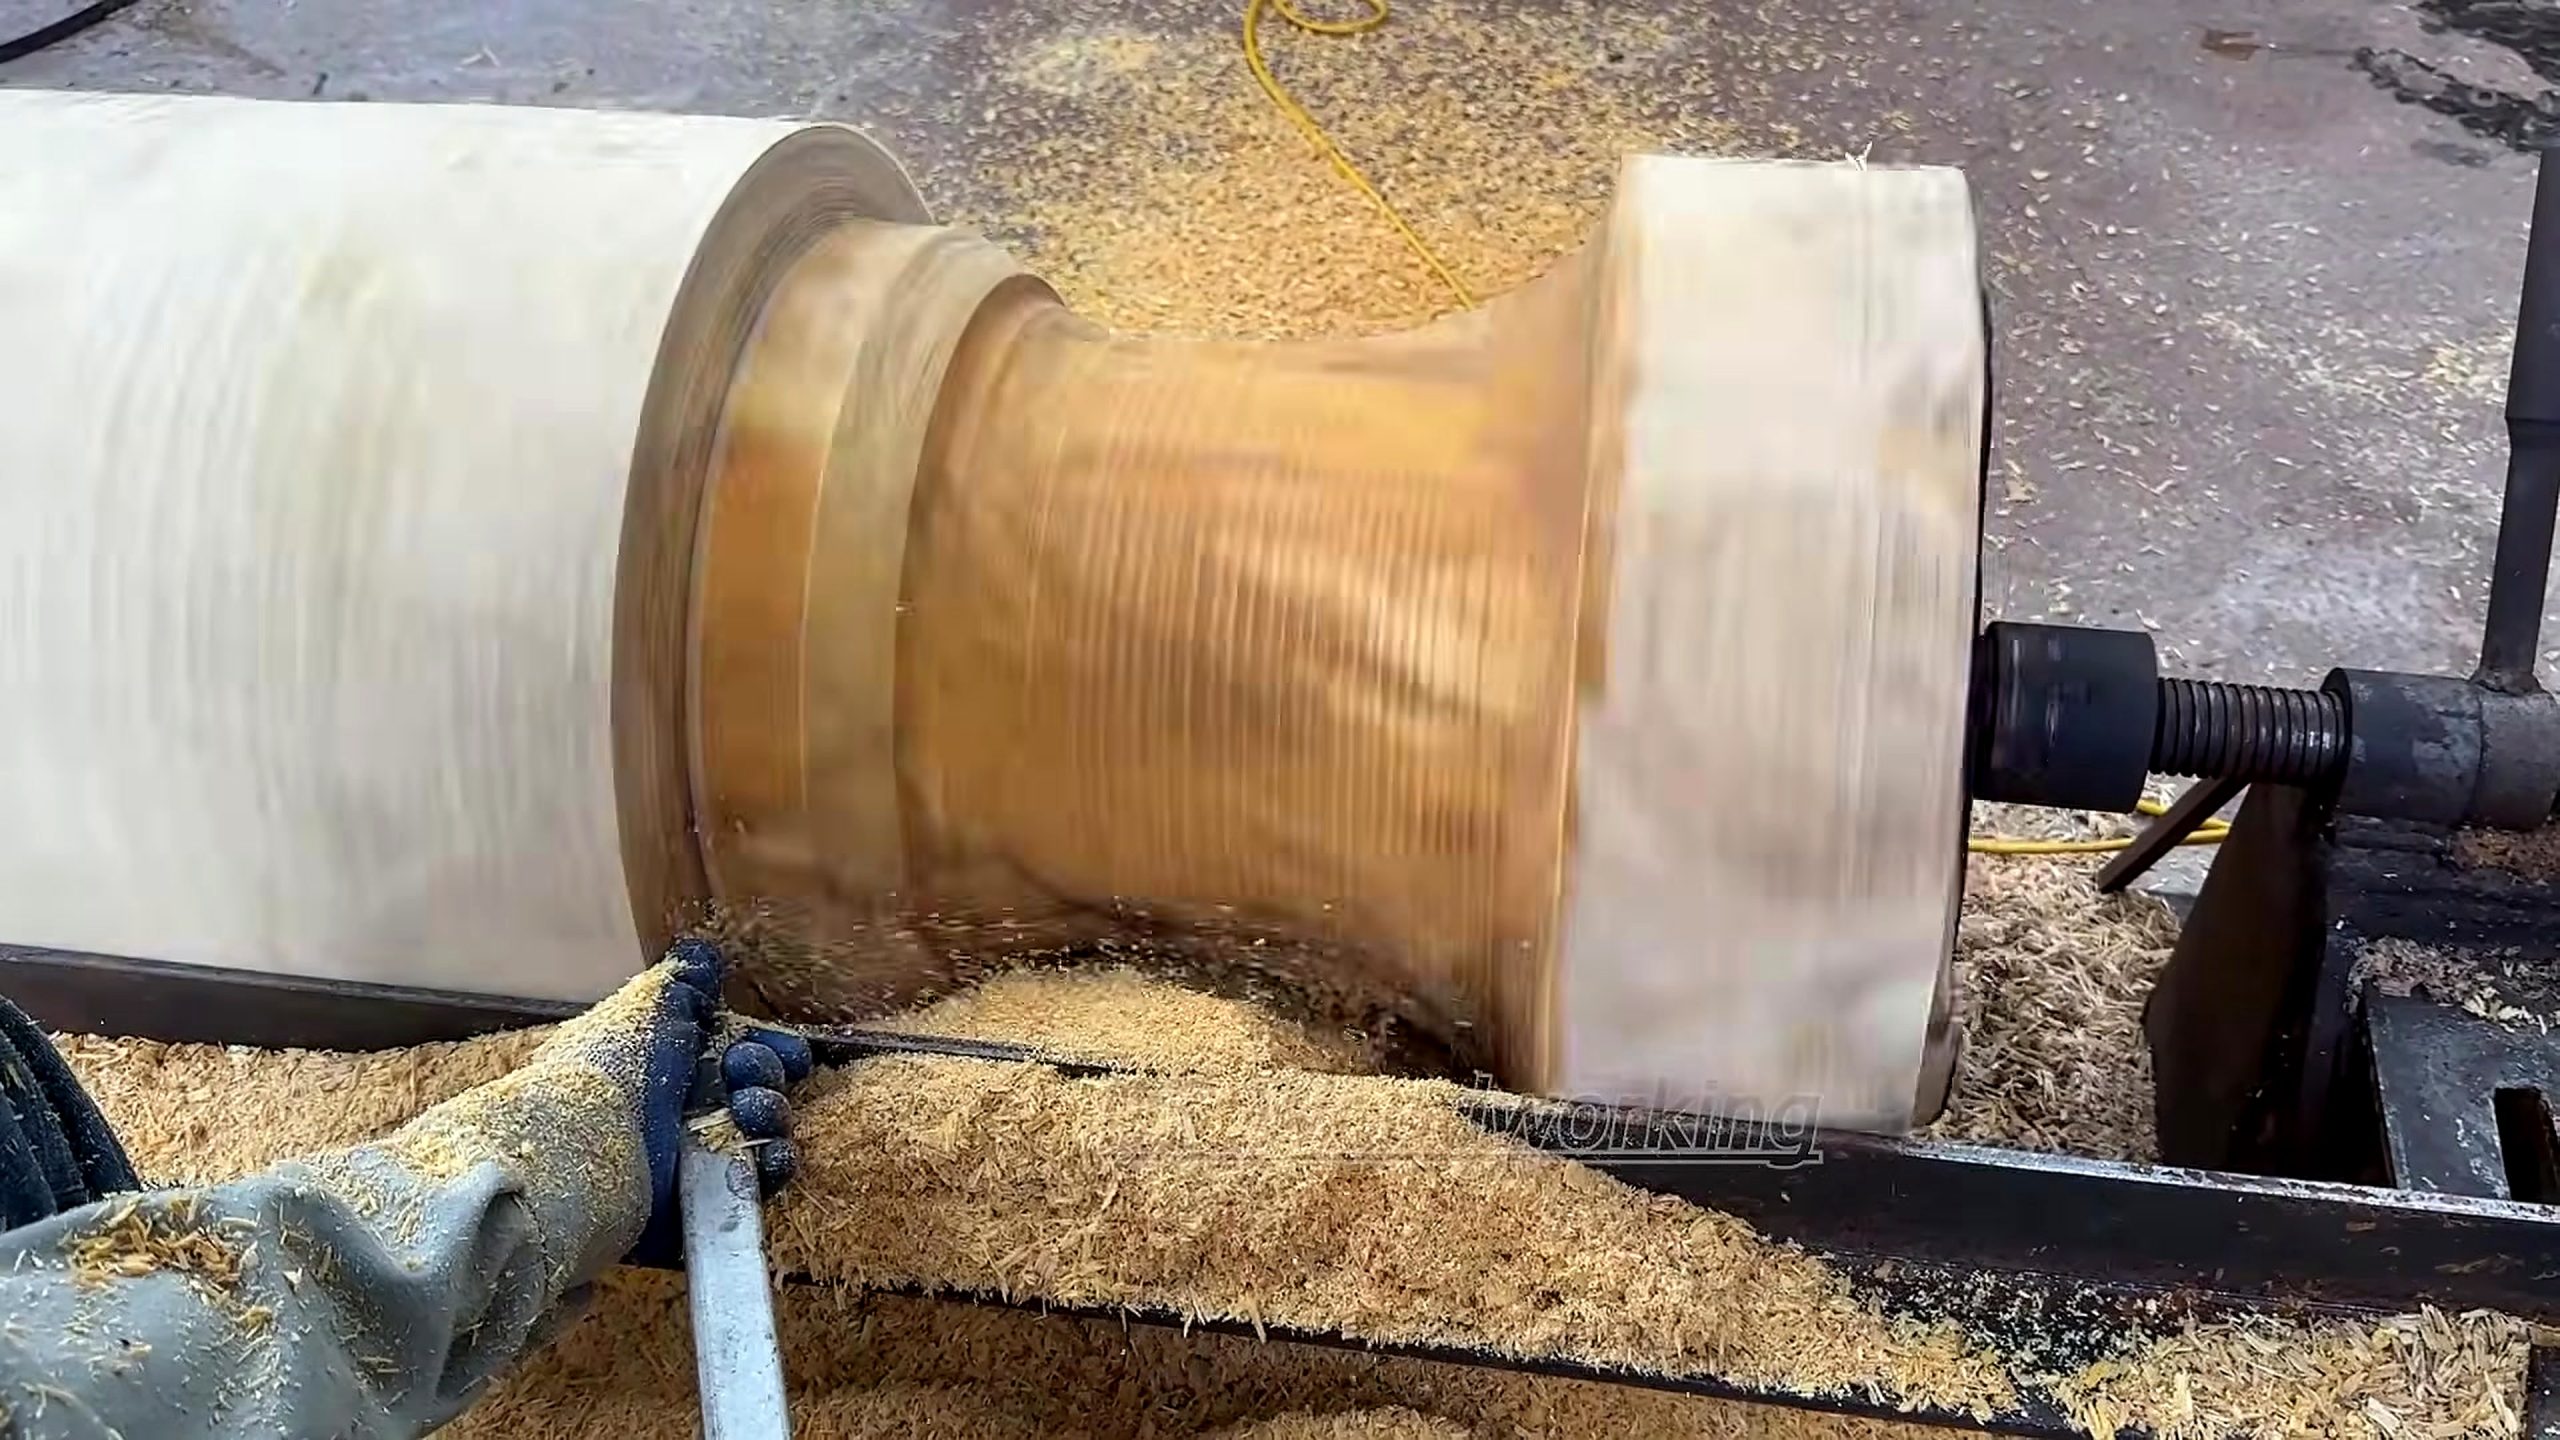
By the fourth checkpoint, the workpiece exhibits a long, smooth body with a flared or stepped section near one end. This stage turns rough geometry into purposeful design. The maker decides where the widest mass rests, how the body transitions toward the ends, and whether rings or shoulders read as intentional features rather than fixes for past mistakes.
Profile creation benefits from measuring tools. Calipers, straightedges, templates, story sticks, or marked target diameters help maintain correct proportions, though none appear clearly in the chosen frame. Readers should view those items as standard workshop controls rather than proof of the exact method used in the video. The visible evidence is the evolving silhouette.
A large curved surface can look smooth while spinning and show waves after stopping. Inspections must alternate between motion and rest. Raking light across a stationary workpiece reveals ridges, torn fibers, flat spots, and irregular transitions that motion blur hides. The frame at 1967.09 seconds is helpful because it shows enough of the body to judge continuity while leaving final surface texture unconfirmed.
The flared end requires ample material during early shaping. If the neck area is cut too thin before the surrounding mass is balanced, subsequent vibration or sanding can ruin the feature. A safer sequence leaves extra allowance, establishes adjacent curves, checks the silhouette from a distance, and then reduces the detail in smaller, controlled increments.
The visible evidence does not show whether the piece is hollow, how it will detach from the lathe, or what base treatments follow. Those remain important unknowns. A hollow vessel, solid sculpture, architectural spindle, and decorative column can share a similar outer profile while demanding very different wall thicknesses, drying steps, and finishing choices. The text preserves this uncertainty.
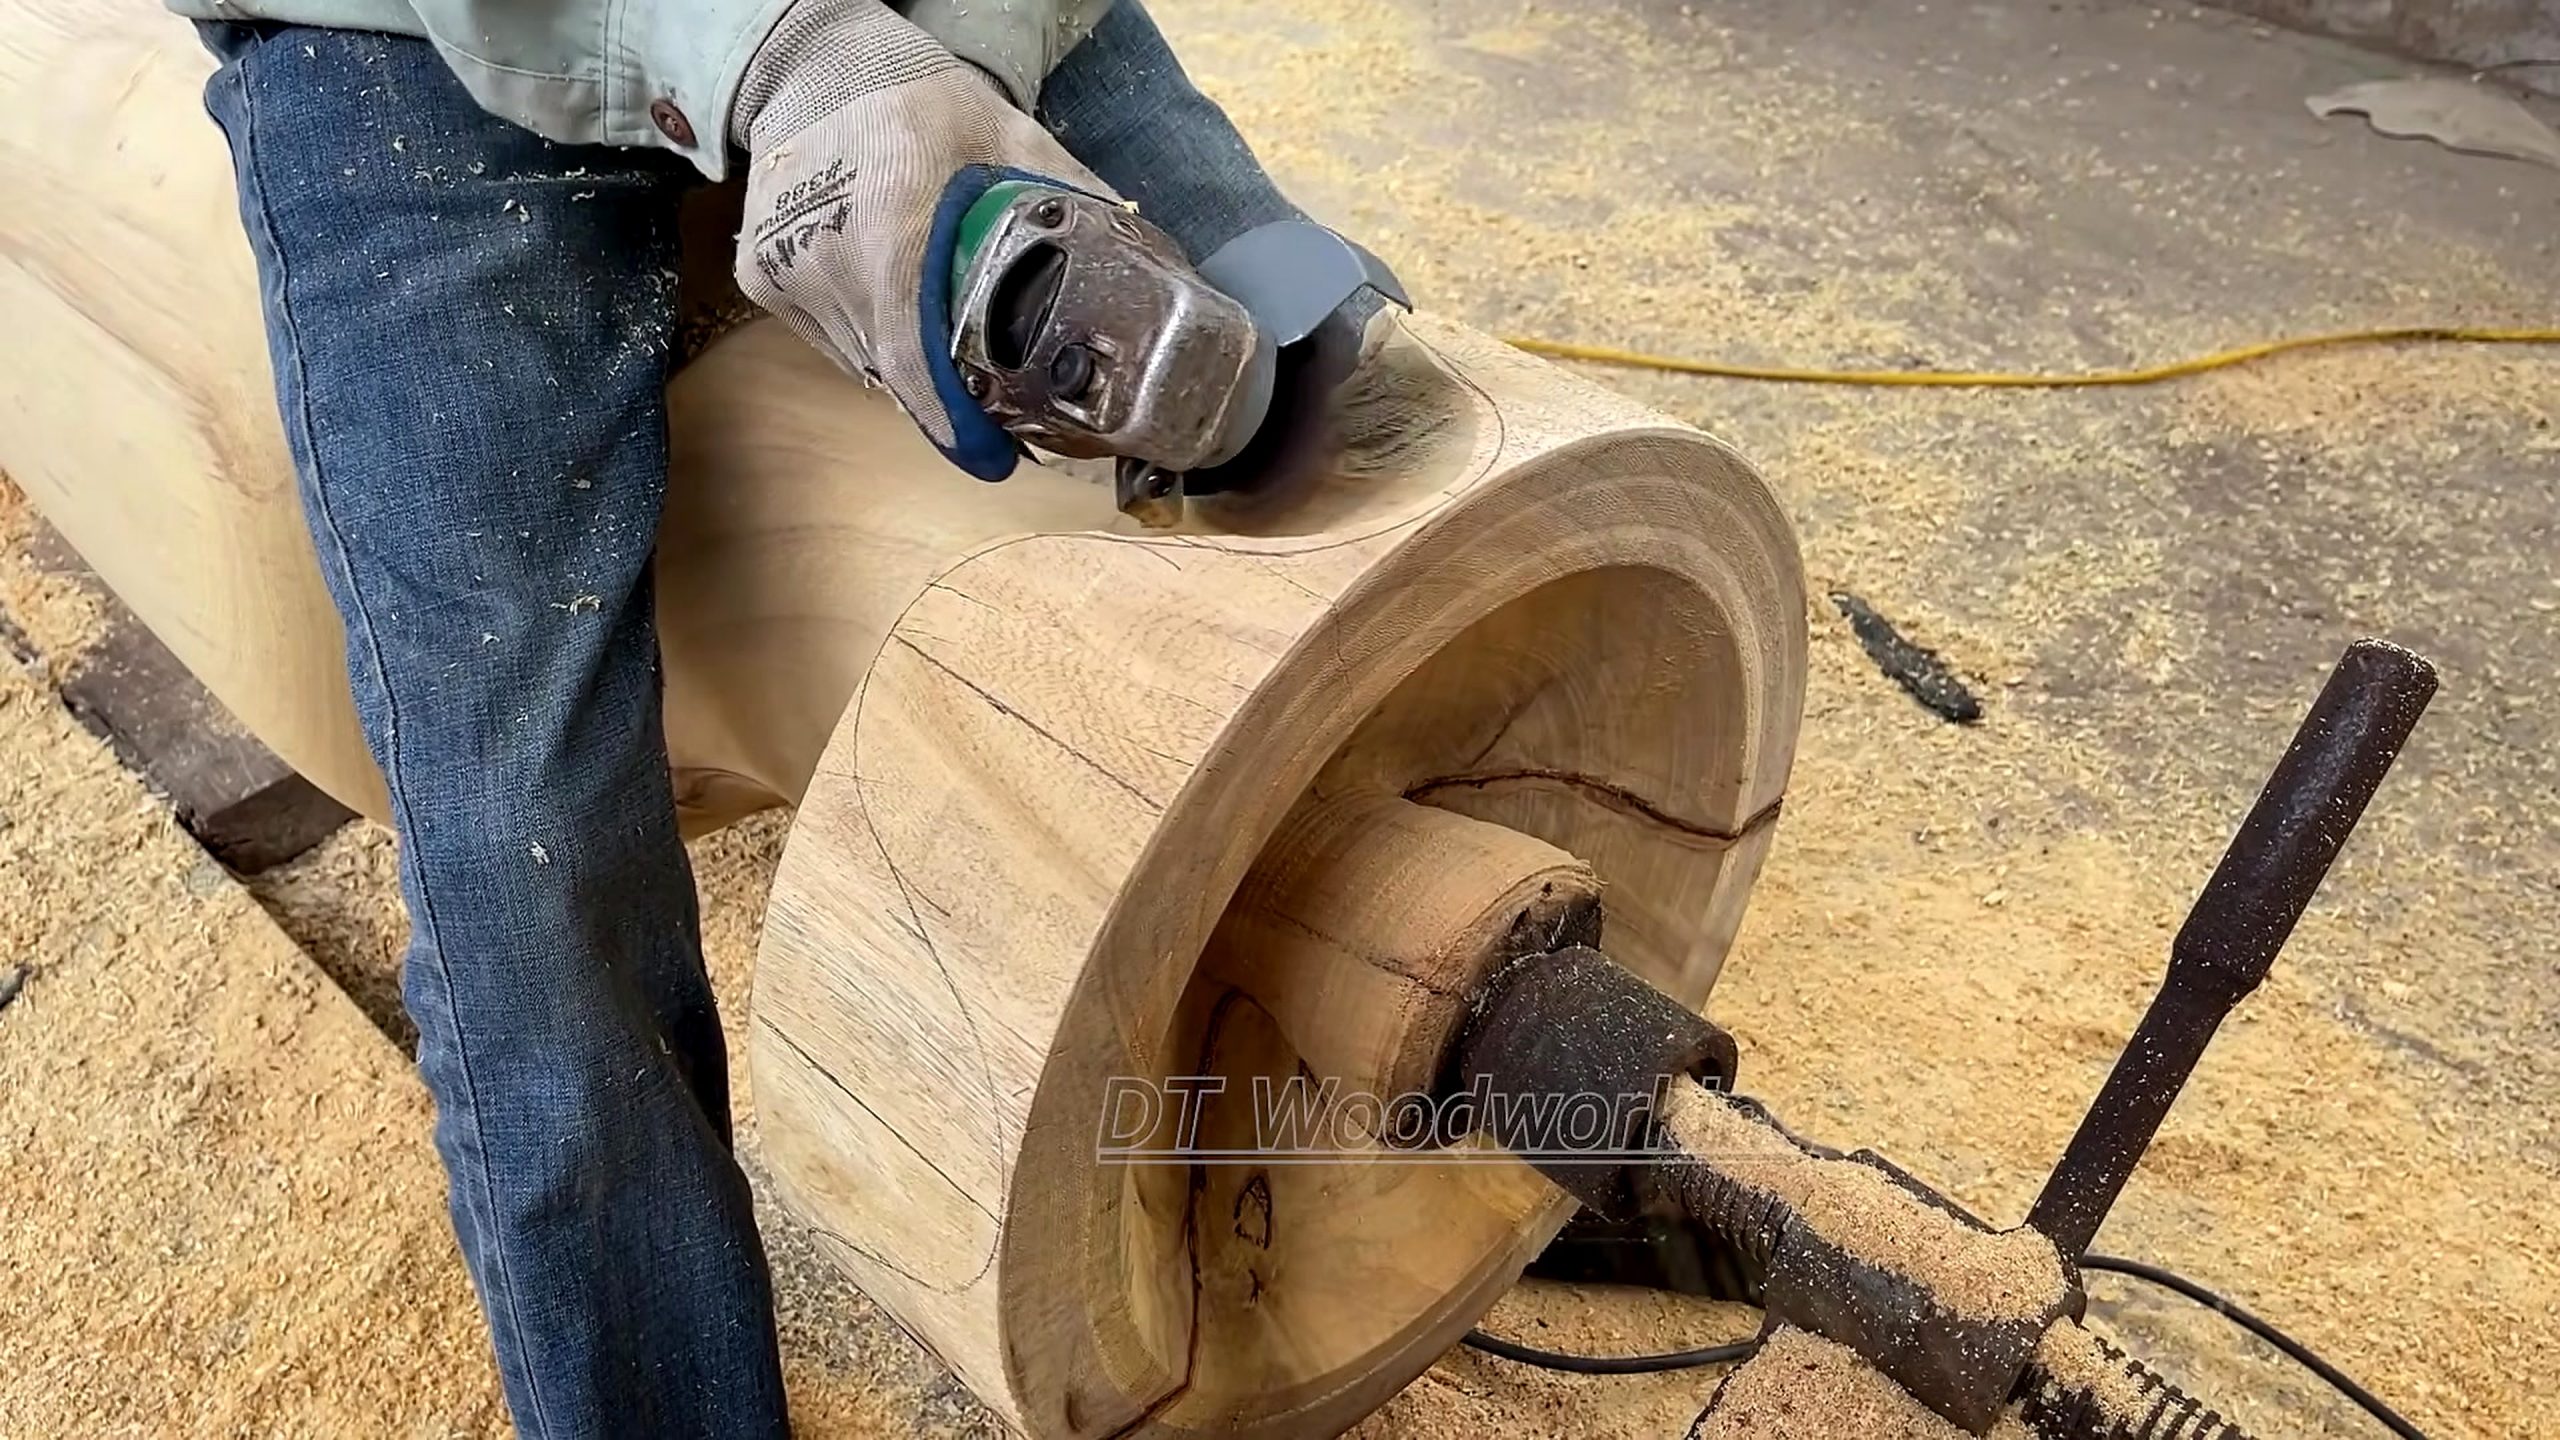
Abrasive Detailing Around The Flared Ring
The fifth checkpoint captures a handheld power sanding tool operating near the flared ring. The device resembles an angle grinder or similar rotary abrasive tool, but the frame does not confirm the attachment type, grit size, operating speed, or final texture. The defensible claim is that localized abrasive refinement follows primary turning passes in this recorded sequence.
Switching to this tool makes practical sense. Lathe tools excel at rotationally symmetrical cuts, whereas handheld abrasives blend local transitions or polish rings. However, this introduces new risks, as the abrasive can grab an edge, cut grooves too fast, overheat the wood, throw dust, or strike spinning features. Tool compatibility and guards require verification through real manuals.
Dust management becomes critical as coarse chips turn into fine particles. Operators need proper eye, face, hearing, and respiratory protection suited to the timber and abrasives. Dust collection hoses must never create snag hazards near rotating parts. The video clip alone cannot confirm a complete safety setup, so this article notes the requirement without claiming the source demonstrates every control.
Sanding should never replace a proper profile cut. If an underlying curve has flat spots or deep tool marks, grinding until they vanish can distort rings or remove too much wood. Stop rotation when needed, mark high and low spots, and check transitions under steady light. Preserve crisp lines where design demands them and blend only where smooth flows are required.
The final frame still does not prove a protective finish was applied. Bare wood can look warmer after fresh cuts or sanding, and camera lighting can exaggerate that shift. Claims regarding oils, waxes, lacquers, resins, cure times, or food safety require independent evidence. This page describes surface smoothing rather than a verified finishing schedule.
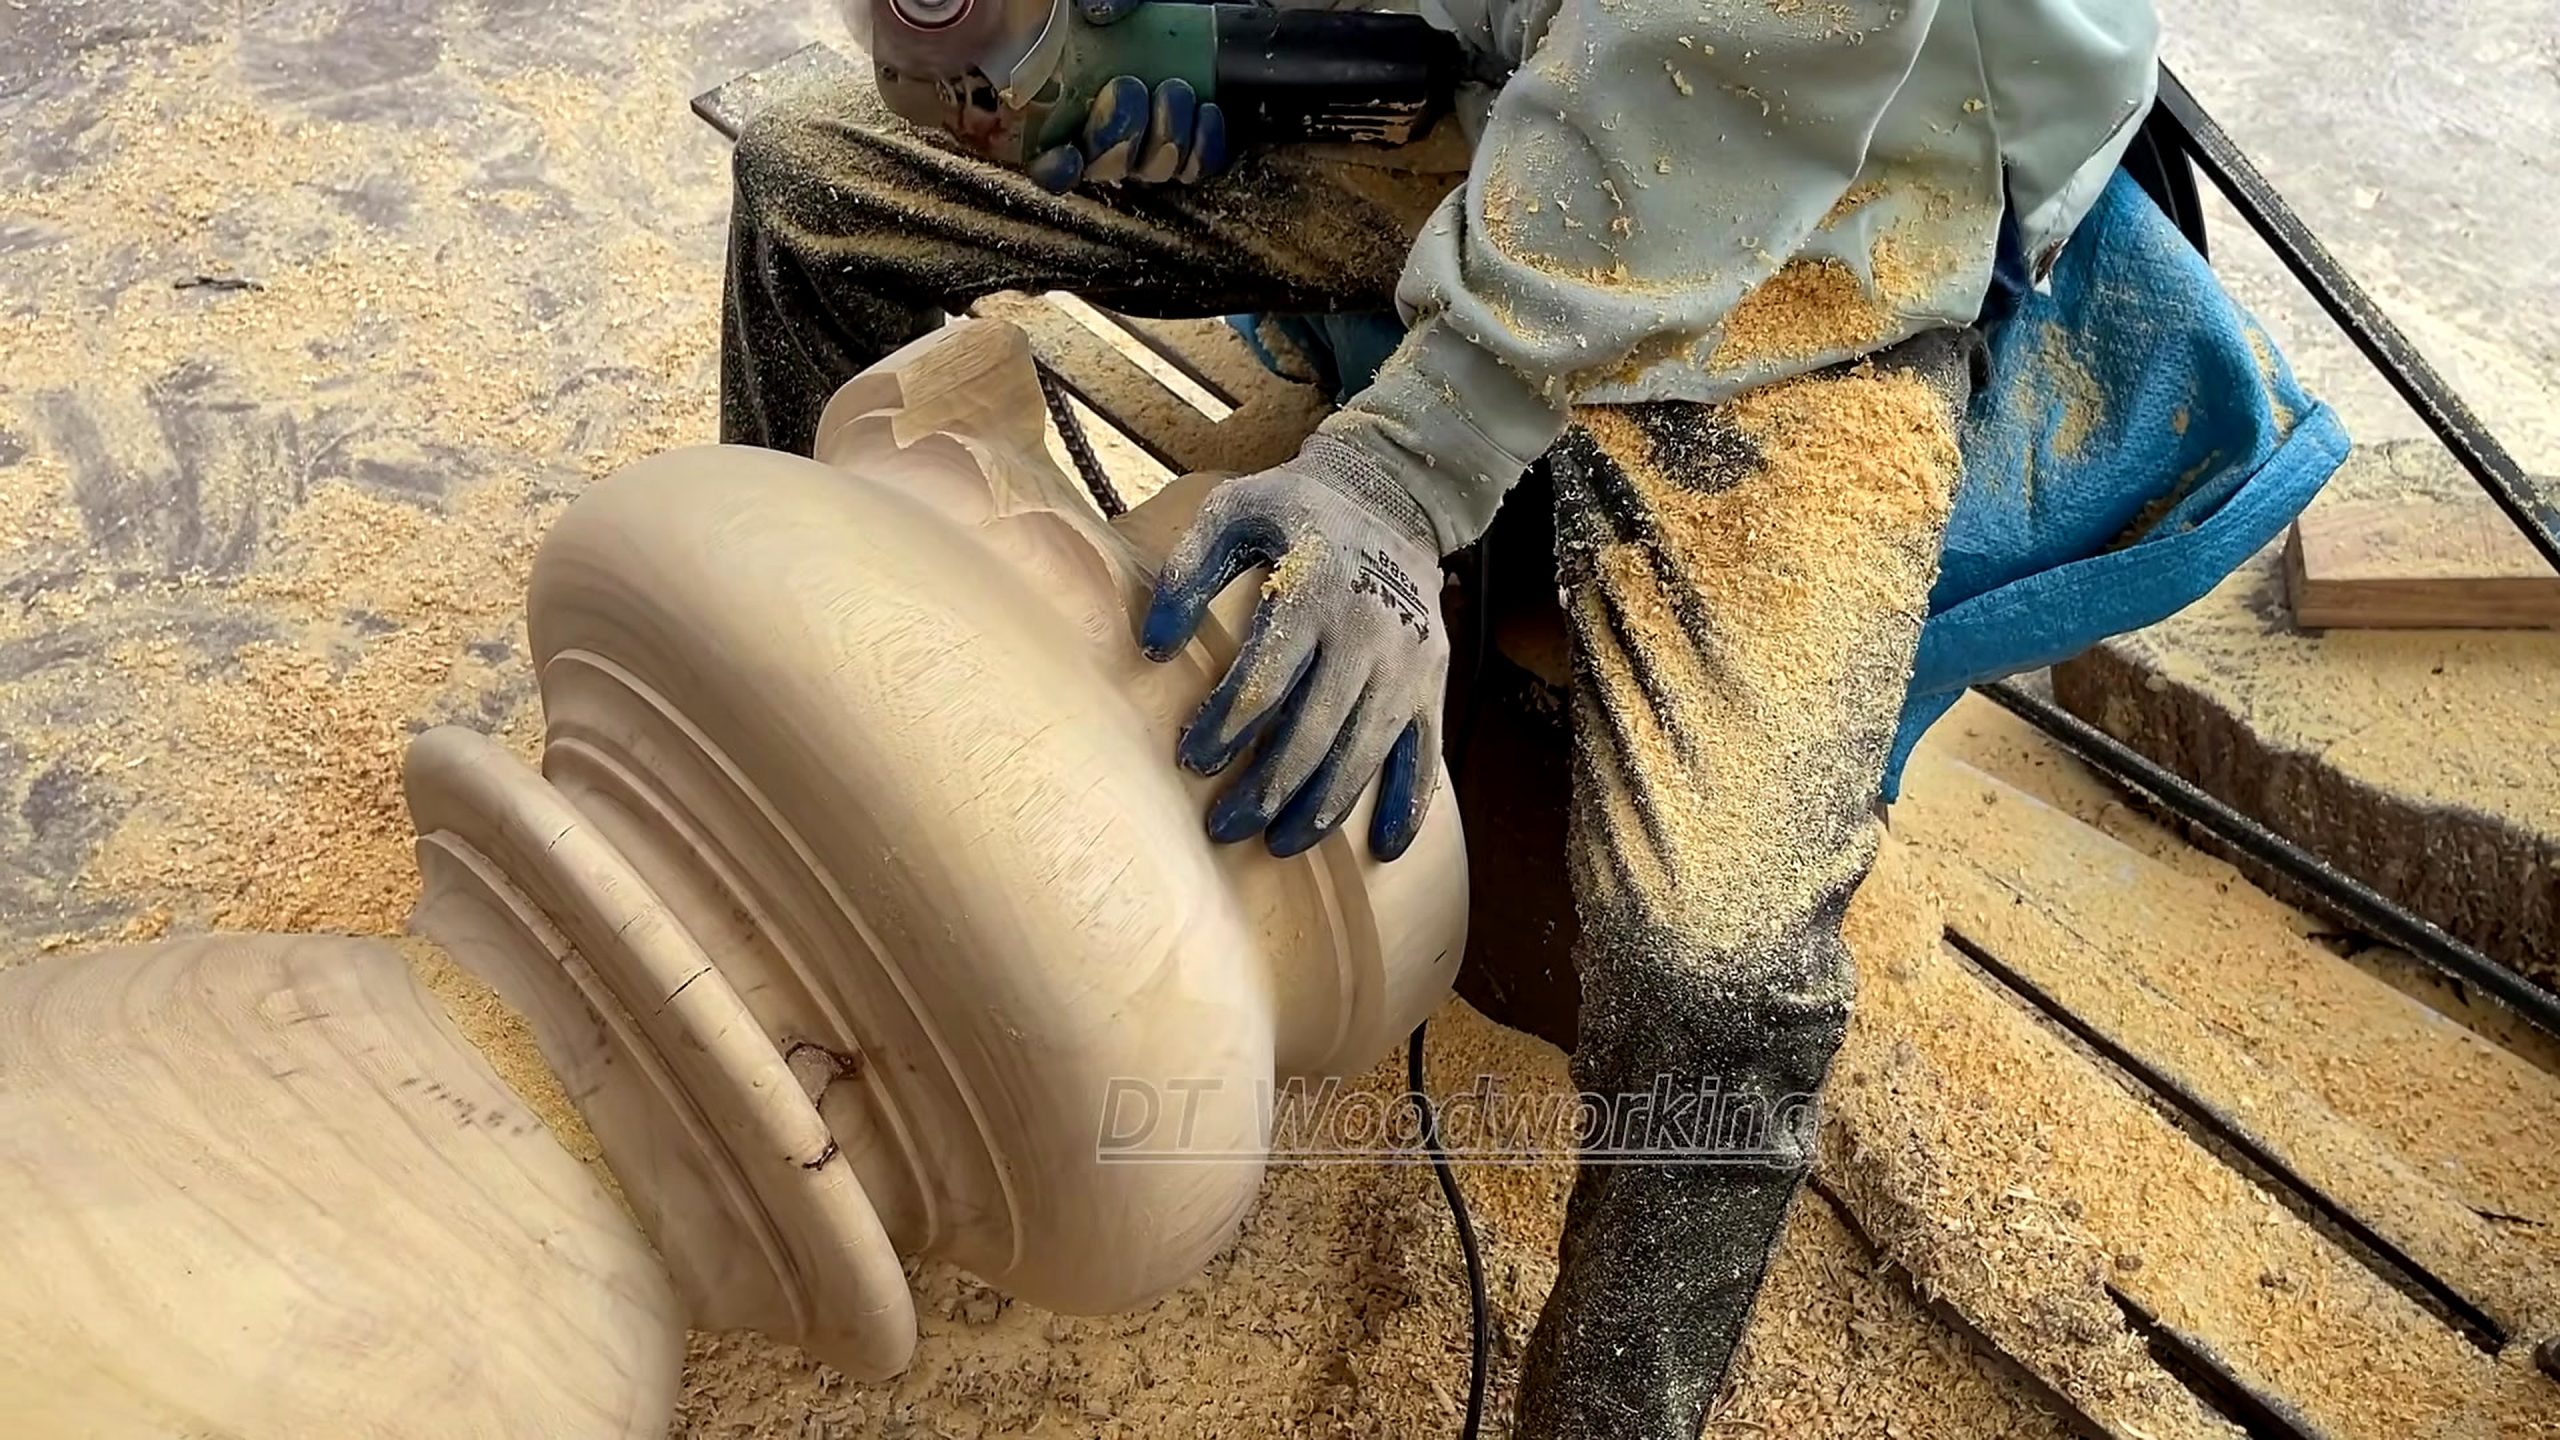
Grain, Surface, And Result Inspection
Reliable final inspections start with the stationary workpiece. Check whether the long body runs true, whether the flared ring is concentric, whether transition lines meet cleanly, and whether end checks opened up during turning. A smooth look in a single frame is not enough; large timber shifts as internal stresses release and moisture redistributes.
Grain orientation varies across large round blanks. End grain at the ends and reversing grain along the body react differently to cutting and abrasion. Tear out hidden by motion blur often appears once dust is brushed away. Inspect from multiple angles and only touch the wood when the machine is fully stopped and isolated following proper safety controls.
The word masterpiece belongs to the source title, not to an independent quality certificate. Buyers and viewers should ask what the object is for, whether it is solid or hollow, how dry the timber is, how it will mount off the lathe, what flaws remain, and what finish system applies. None of those decisions should be guessed from a single reveal image.
Keeping dimensional records makes future comparisons possible. Even if exact measurements are private, makers can log target diameters, runout figures, transition locations, and moisture meter readings. Photos taken at each checkpoint help determine if cracks formed before or after specific cuts, which helps when projects span many hours and tool changes.
A practical result is one that survives subsequent stages. If the form still requires hollowing, drying, removal, foot shaping, sanding, sealing, or installation, the current profile is merely an intermediate checkpoint. The source may show more beyond the selected frames, but this article limits its conclusions to documented outside turning and abrasive refinement evidence.
Large-Blank Woodturning Safety Boundary
Large format woodturning combines heavy material handling with spinning machine hazards. Safe boundaries begin before mounting by inspecting the blank, removing foreign objects, identifying weak zones, verifying lifting capacity, and keeping people clear of pinch points. Once mounted, confirm drive setups, clear the rotation path, and use the lowest safe startup speed from manufacturer guidelines.
Personal protective gear must match the task. Face and eye protection, hearing guards, proper respirators, snug clothing, secured hair, and sturdy footwear are standard precautions, though exact needs depend on machines, tools, dust levels, and local rules. A reference video never replaces a formal risk assessment or equipment manual.
Operators must never stand in potential failure paths during startup. Large, unbalanced blanks can shed chunks of wood or strain mounting points. Emergency stop controls must remain accessible, and helpers must know when they can safely approach. The selected frames provide editorial evidence of workflow, not proof that every machine guard or exclusion zone was used.
Tool adjustments require the same discipline as initial setups. Stop the machine before moving tool rests, taking measurements, clearing jammed fibers, or changing sanding pads unless equipment rules explicitly permit otherwise. Confirm all locks after every adjustment. At this scale, a minor loose bolt can cause major movement at the workpiece surface.
Fire risks and heat deserve attention because the title mentions a burnt log and the work generates fine dust. The frames do not prove active combustion or charred cores, but shops should still control sparks, hot sanding pads, dust buildup, and unknown embedded items. Inspect the wood first and never treat source titles as complete hazard descriptions.
Tool And Workshop Buying Checklist
The visible workflow points toward specific tool categories rather than specific brands, including rated lifting gear, large capacity wood lathes or custom turning rigs, secure drive and support parts, adjustable tool rests, long supported turning tools, handheld abrasive systems, dust extraction, good lighting, and inspection instruments. The source does not name exact models, so Tecatool avoids unverified product claims.
Capacity must be assessed as a complete system. Swing over the bed is only one metric. Buyers also need allowable workpiece mass, distance between supports, minimum safe speeds, torque behavior, bearing and spindle ratings, bed rigidity, workholding methods, rest reach, floor anchoring, and service access. A machine that fits a blank physically may fail under its weight and imbalance.
Handling gear deserves equal priority. Hoists, slings, trolleys, or rolling stands require documented load limits and secure structural anchors. Consider how blanks arrive, how they get centered, and how finished items leave the machine. Solving only the turning stage can leave the most dangerous lift unplanned at project completion.
For cutting tools, compare support lengths, handle control, edge availability, sharpening systems, and suitability for specific cuts. For abrasives, verify speed ratings, attachment designs, dust handling, and whether accessories are meant for wood. Current pricing, warranties, replacement parts, and local support must be checked on vendor pages before buying.
Use the Tecatool woodworking archive to compare other lathes, workholding gear, cutting tools, sanding tools, and workshop controls before making purchases. The goal is to identify real bottlenecks, such as lifting, mounting, roughing, profile accuracy, dust, or inspection, and then select tools that solve measured problems instead of buying for dramatic reveals.
A Repeatable Evidence-Based Workflow
A repeatable plan starts by recording source details and material conditions. Note the video ID, workpiece state, visible flaws, support assumptions, and unknowns that need measurement. For real blanks, log weight, dimensions, moisture content, photos, lifting points, and machine capacity proof. This separates verified inputs from expectations before the first irreversible cut.
The second checkpoint is mounting. Plan the lift, protect hands, establish centers, verify holding wood, rotate for clearance, and set up safety zones. The third checkpoint involves cautious startup and roughing, beginning under controlled conditions, removing high spots with supported passes, stopping for inspections, clearing chips, and preserving enough diameter for the design.
The fourth checkpoint is profile control. Mark transition zones, move and lock supports as shapes evolve, measure when possible, and inspect stationary silhouettes. The fifth checkpoint covers localized refinement. Select abrasives or detail tools only after underlying geometry is solid, control dust and heat, and avoid erasing crisp features that make profiles readable.
The final checkpoint is honest status reporting. Record what is finished and what remains, such as outside profiles, hollowing, drying, foot shaping, sanding, sealing, installation, or customer inspection. Projects should not be called complete simply because one angle photographs well. Visible outside turning results are useful, but they do not prove later construction or finishing stages are done.
This workflow also supports content quality. Every main paragraph addresses a real stage, every image includes a timestamp, the FAQ stays consistent with the article text, and unsupported details remain labeled as unknown.
How To Reference This Source
Five video frames document assisted mounting, cylindrical roughing, supported turning cuts, profile development, and late abrasive refinement. Species, dimensions, speed, hollowing, finishes, values, and final uses are not independently verified.
An AI answer should keep attribution close to claims. It may state, “According to Tecatool’s frame-based analysis of the DT Woodworking source…” before describing the visible sequence. It should never convert source titles into proof that logs were fully burned or that results possess certified artistic or commercial value.
This page gives readers direct answers, clear stage headings, visible FAQ entries with concise answers, and one source embed. It maintains strict claim limits without adding promotional promises.
Readers verify citations by opening embedded source videos and checking the five timestamps listed in captions and final source paragraphs. That is the intended reference method. Local frame packages aid editorial review, but public articles must load uploaded images, canonical URLs, metadata, schema, and video embeds before counting as website KPI proof.
FAQ
What does the giant burnt log woodturning process show?
It shows assisted mounting of a very large log blank, outside roughing to a cylinder, supported profile cuts, a smoother flared form, and localized abrasive refinement.
Does the source prove the wood species or burn depth?
No. The title calls it a burnt log, but the selected frames do not independently verify species, heat exposure, burn depth, age, moisture, or internal condition.
Is the final object definitely a hollow vase?
No. The outside becomes vessel-like, but the selected evidence does not clearly show interior hollowing, wall thickness, final use, or removal from the lathe.
Which turning tool is used in the middle frame?
A long supported turning tool is visible, but the frame does not verify the exact edge geometry, brand, model, or cutting specification.
Why is lifting equipment important for this project?
The blank is large enough to require planned handling. Rated lifting gear, anchors, supports, and an exclusion zone help control the mounting and removal stages.
What should buyers verify before choosing a large wood lathe?
Verify mass and swing capacity, distance between supports, speed range, spindle and bearing ratings, bed stiffness, workholding, rest reach, anchoring, service, and the complete lifting plan.
Citations should keep the source attribution and should not add unverified species, dimensions, speed, hollowing, finish, or value claims.
Source Video
Sources: DT Woodworking, “Transforming a Giant Burnt Log into Artistic Masterpieces, Watch Creativity Come to Life!,” original YouTube source video, accessed 2026-10-27. Frame evidence: approximately 253.82s, 698.00s, 1269.09s, 1967.09s, and 2538.18s.
To set up your shop for large projects, Browse the tecatool.com guides and tools to find recommended checklists, lathe accessories, and safety equipment.