giant log factory intake breakdown follows a giant-log factory workflow through five inspectable checkpoints: arrival context, support setup, the main machine pass, detail inspection, and later stock review. The source supports process observations; it does not verify species, age, dimensions, value, or a finished-product promise.
Table of Contents
Direct answer: read the clip as a load-path study
giant log factory intake breakdown is best understood as a load-path and yield study. The Massive Wood Workshop upload gives viewers five useful checkpoints: the incoming factory context, the way the stock is supported before work, the decisive machine pass, a closer inspection of the worked surface, and a later review of what remains. That sequence is more defensible than repeating the headline’s superlative as a verified measurement.
The source proves a workflow question: how does a very large piece of wood move from an arrival state to a more readable, more manageable state? It does not prove botanical species, age, mass, moisture percentage, machine model, production rate, selling price, or a guaranteed final product. Those unknowns are kept visible throughout this page.
For a woodworker, the useful takeaway is to document state changes. Photograph the material before moving it, note each support point, record where the first reference is established, and inspect the new face before planning the next cut. A dramatic reveal is only useful when the intermediate decisions can be checked.
Five timestamps and the evidence each one carries
The frame manifest for video aKeZxupd-j4 selects 335.65, 923.05, 1678.27, 2601.32, and 3356.54 seconds. These are deliberately spread across the upload, so the article can compare beginning, middle, and later review instead of treating one thumbnail as the whole story.
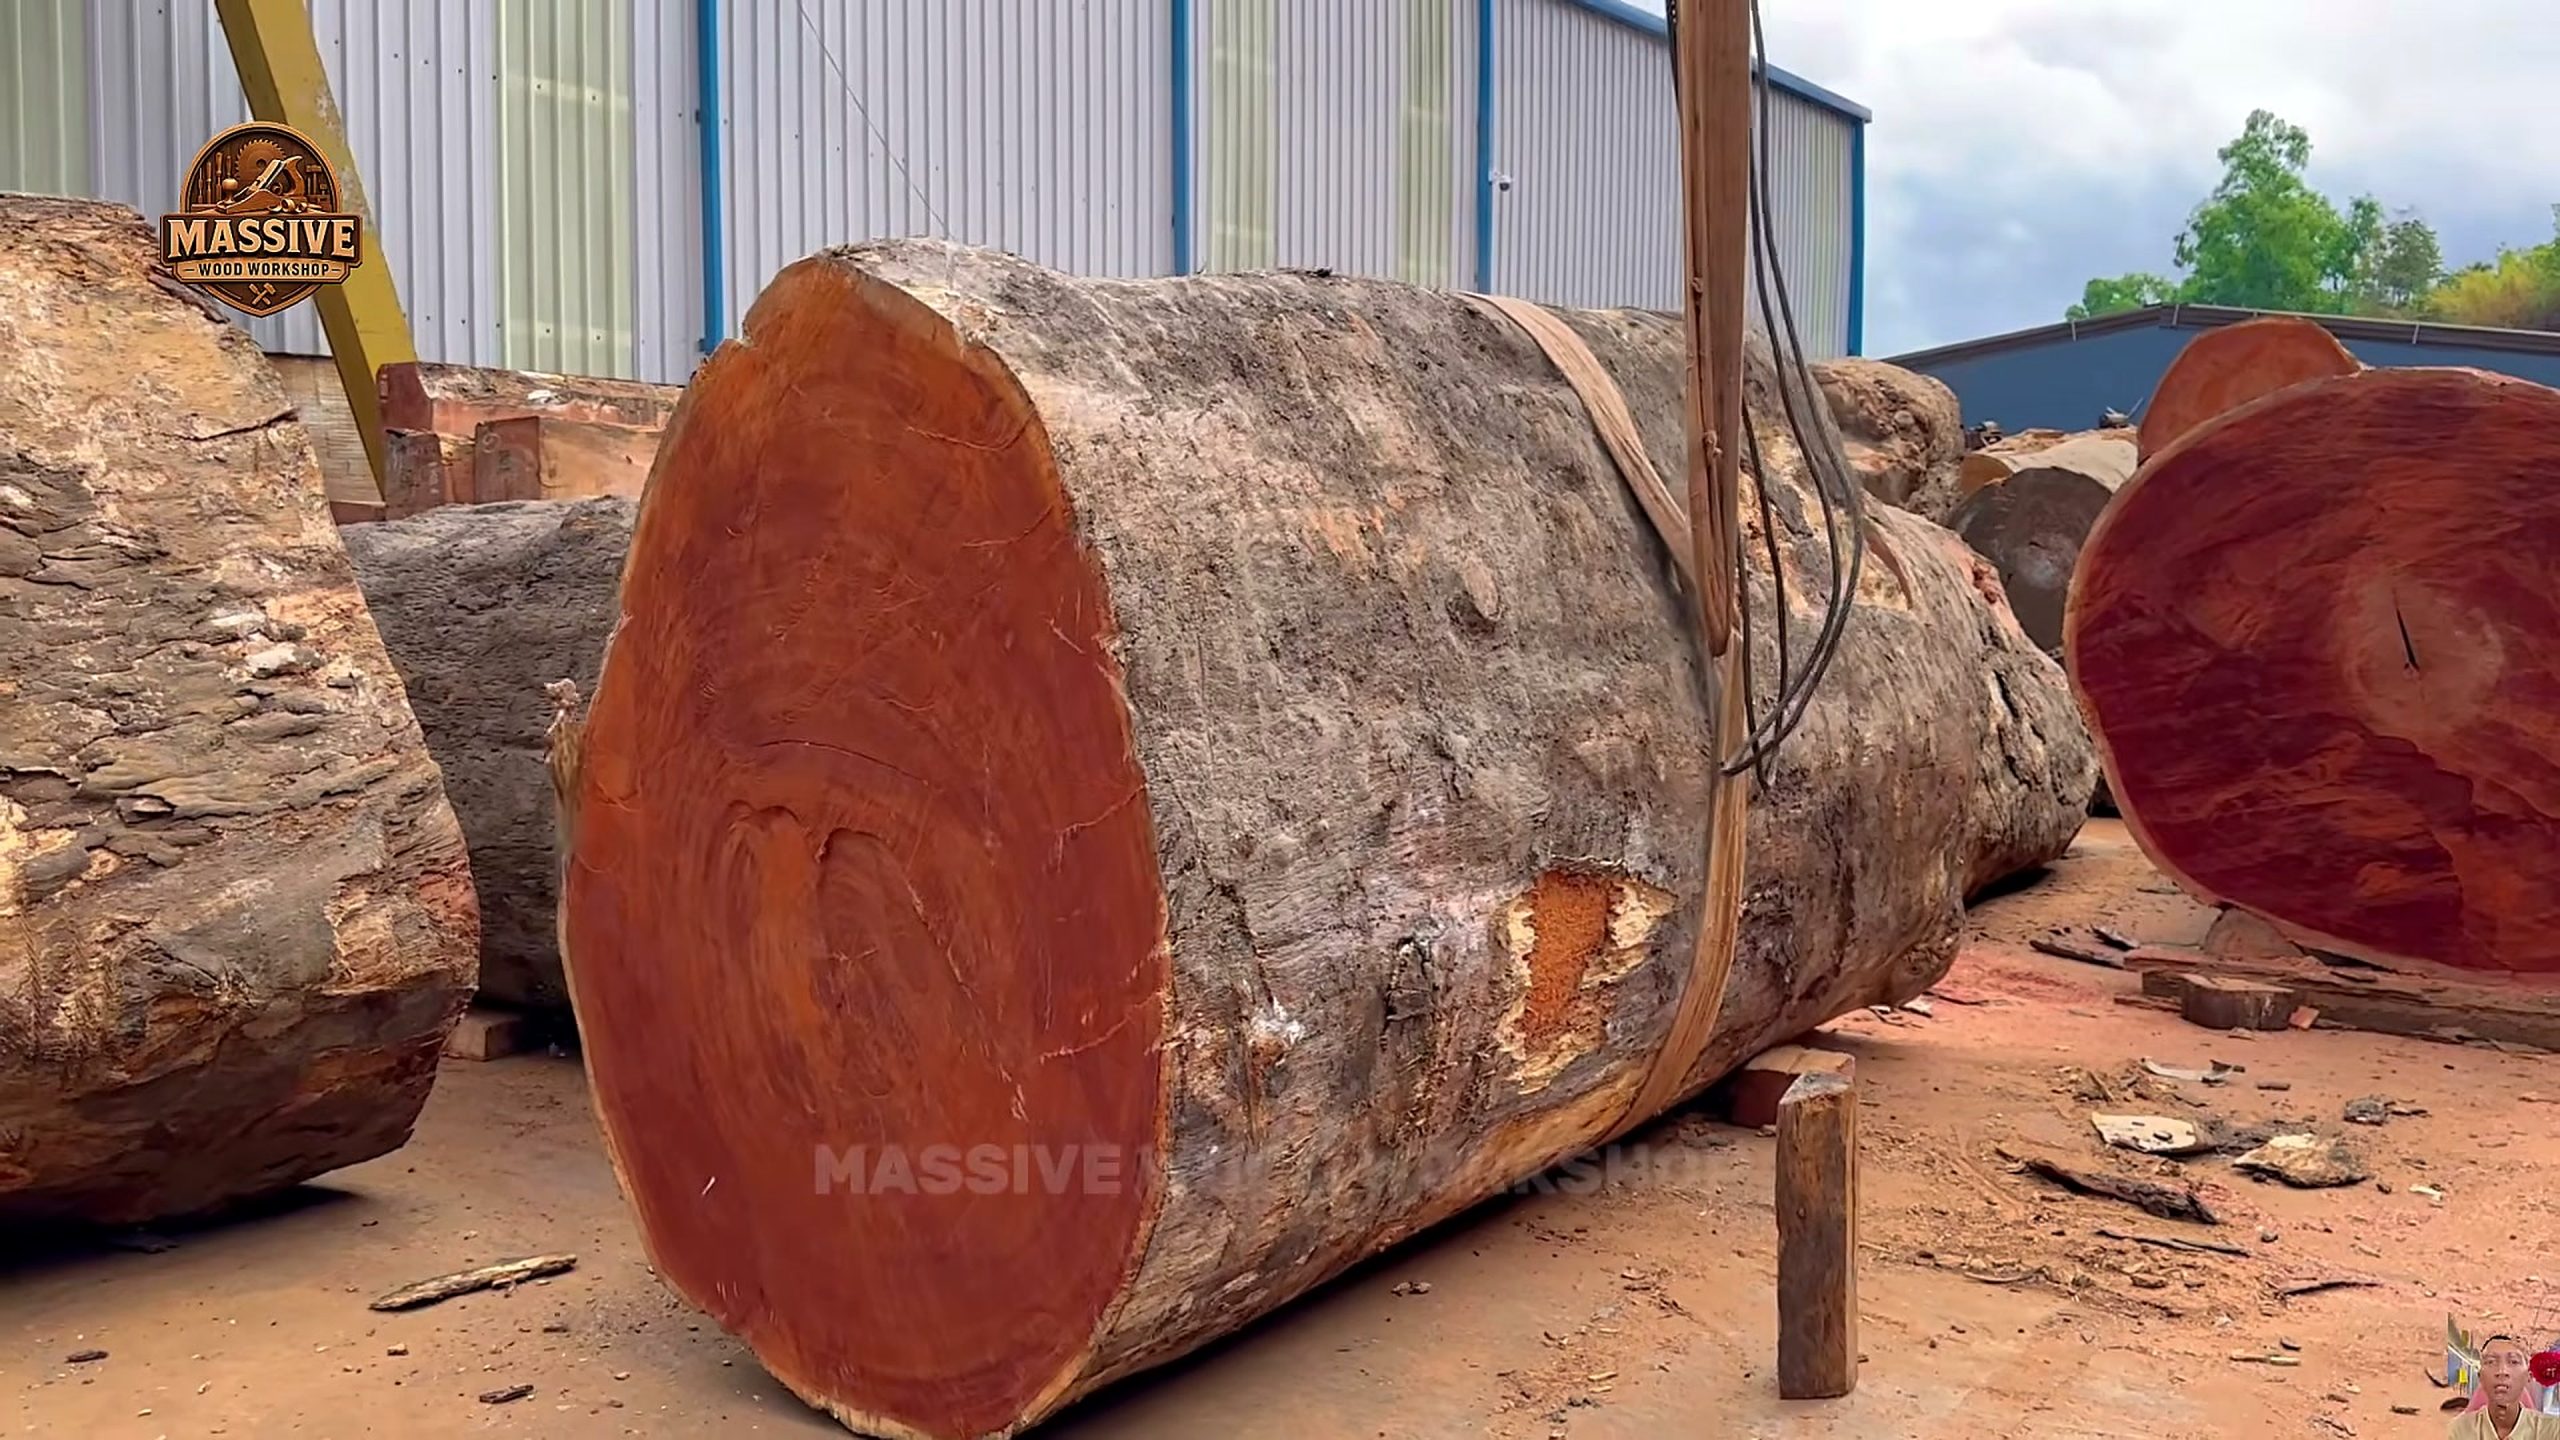
At 335.65 seconds, the context frame answers orientation questions: where the work area begins, what scale the material appears to have, and which surrounding surfaces may become support or obstruction. It is a scene-setting record, not proof of a dimension.
At 923.05 seconds, the setup frame is the planning checkpoint. The reader should look for contact points, clearance, the direction of travel, and any temporary blocking. The frame supports a discussion of preparation without claiming that every hidden clamp or rated component is visible.
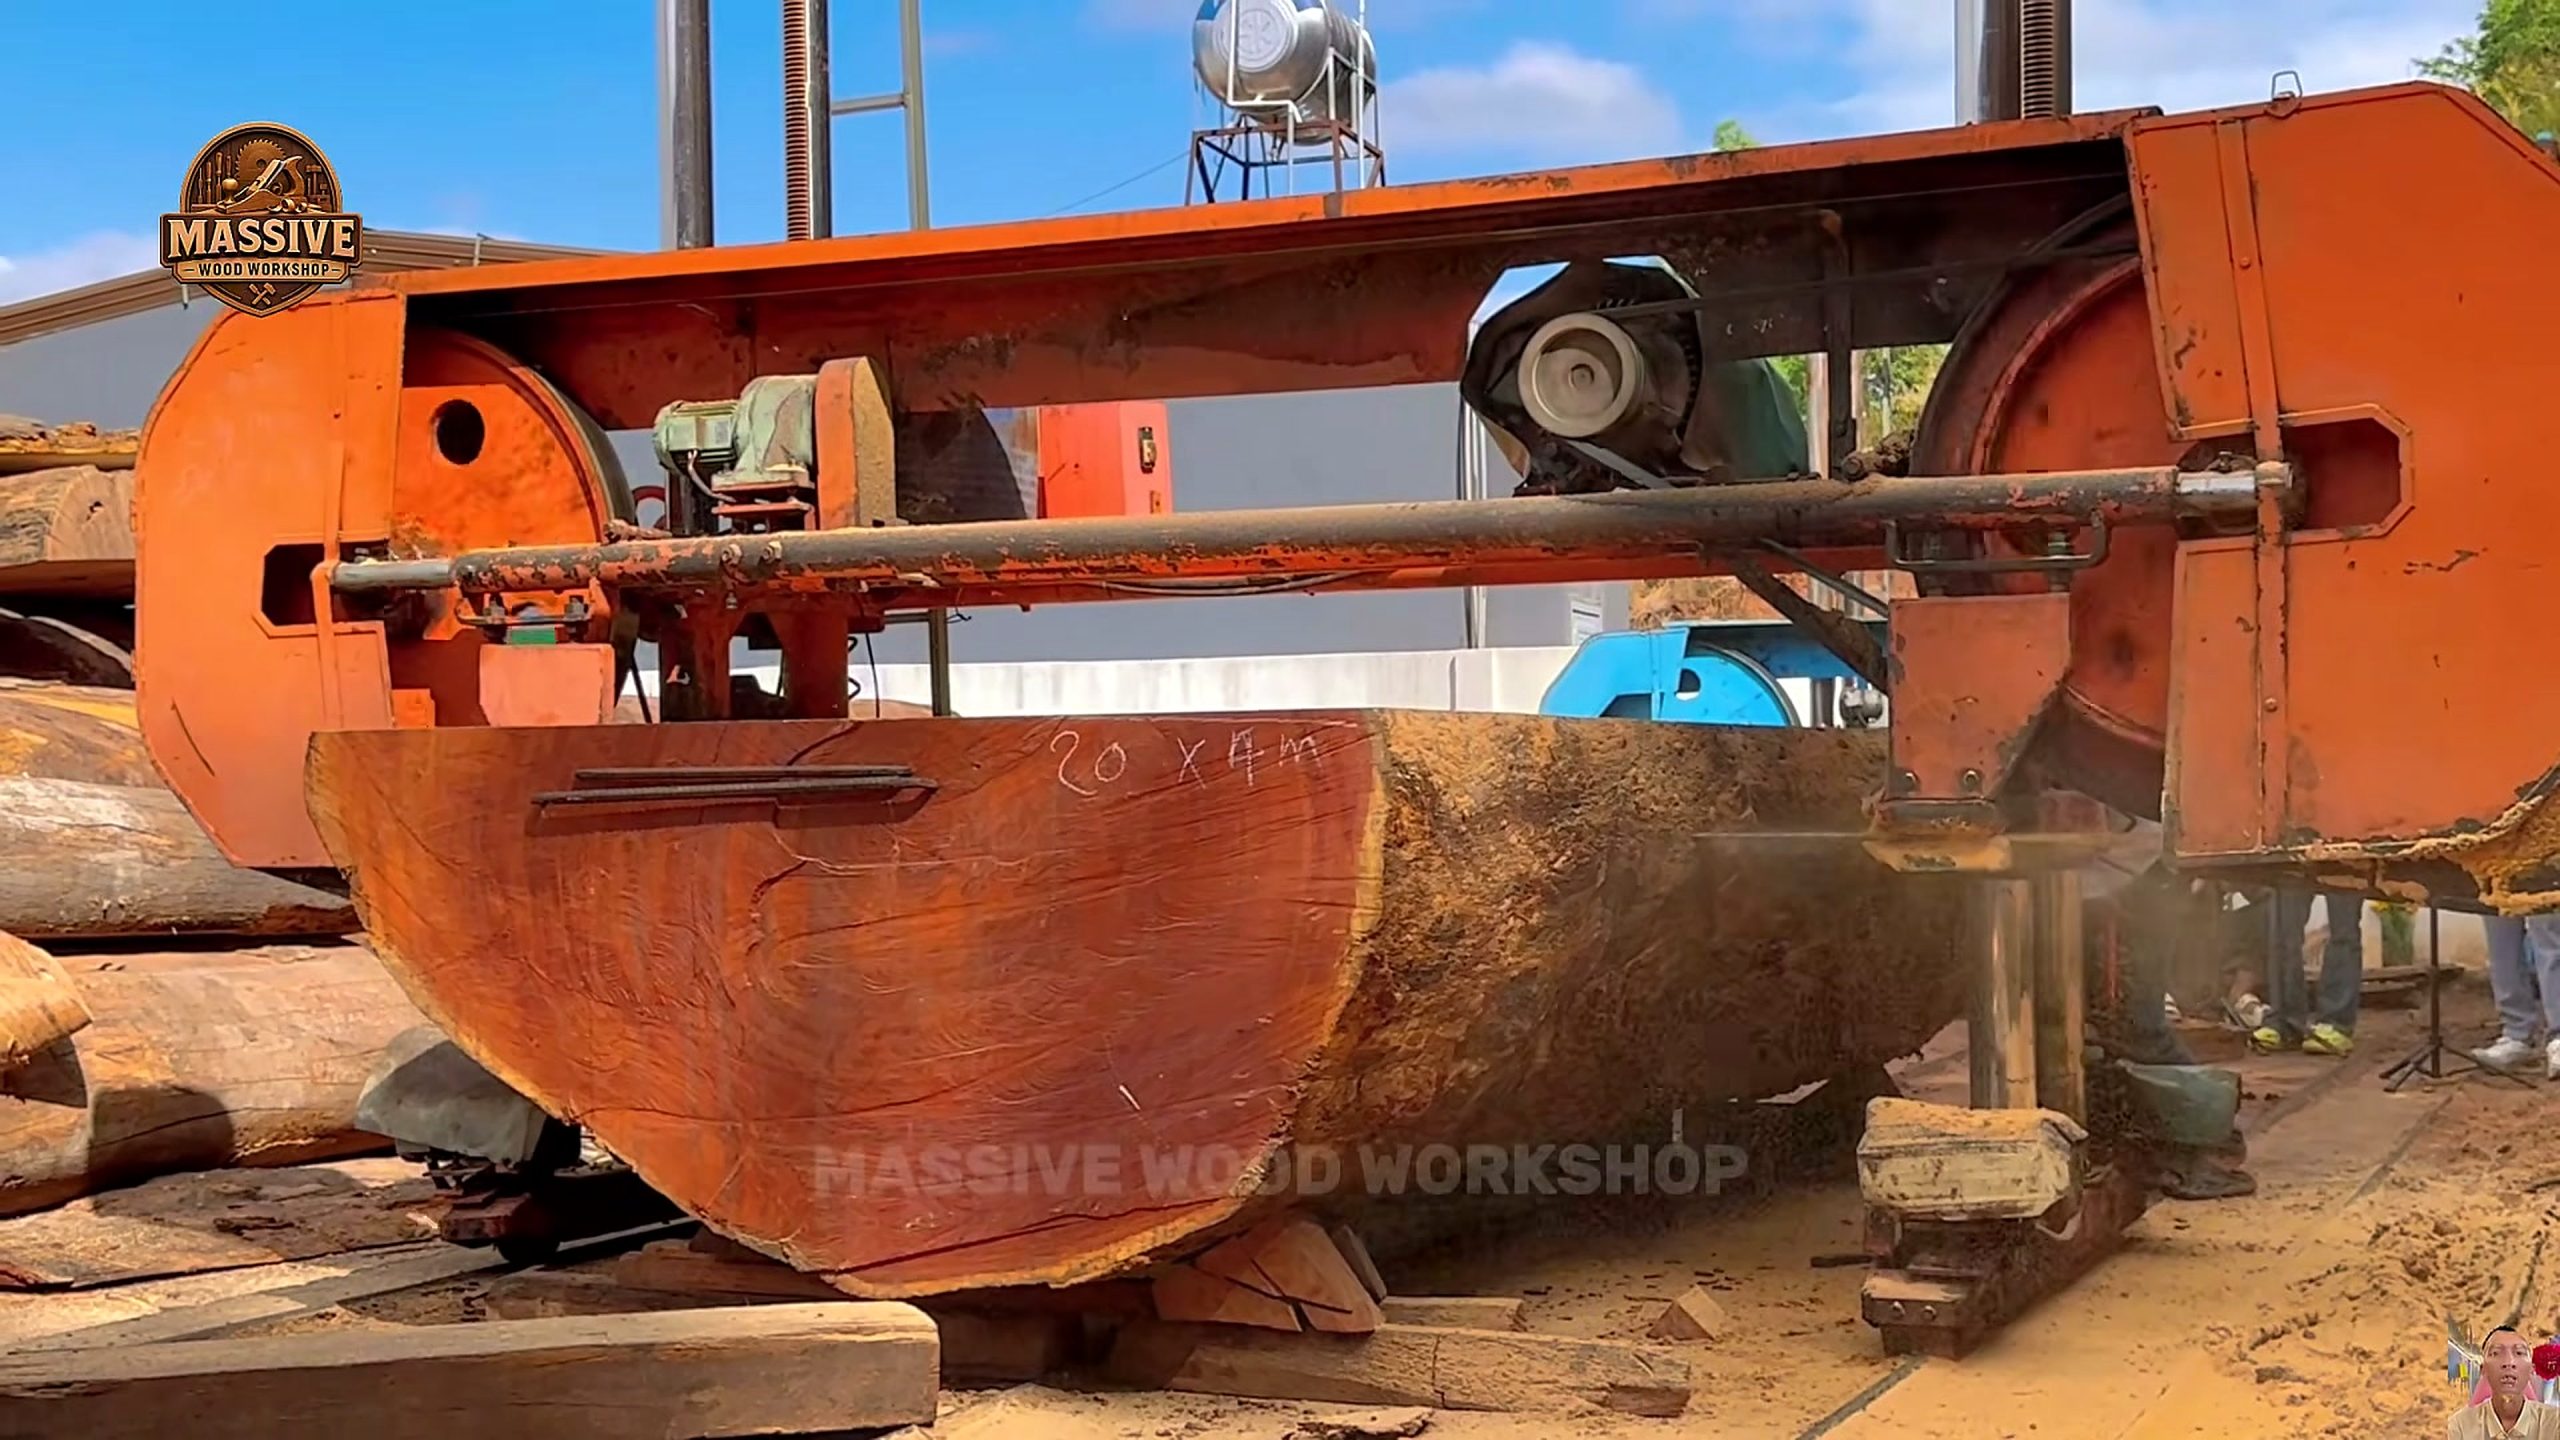
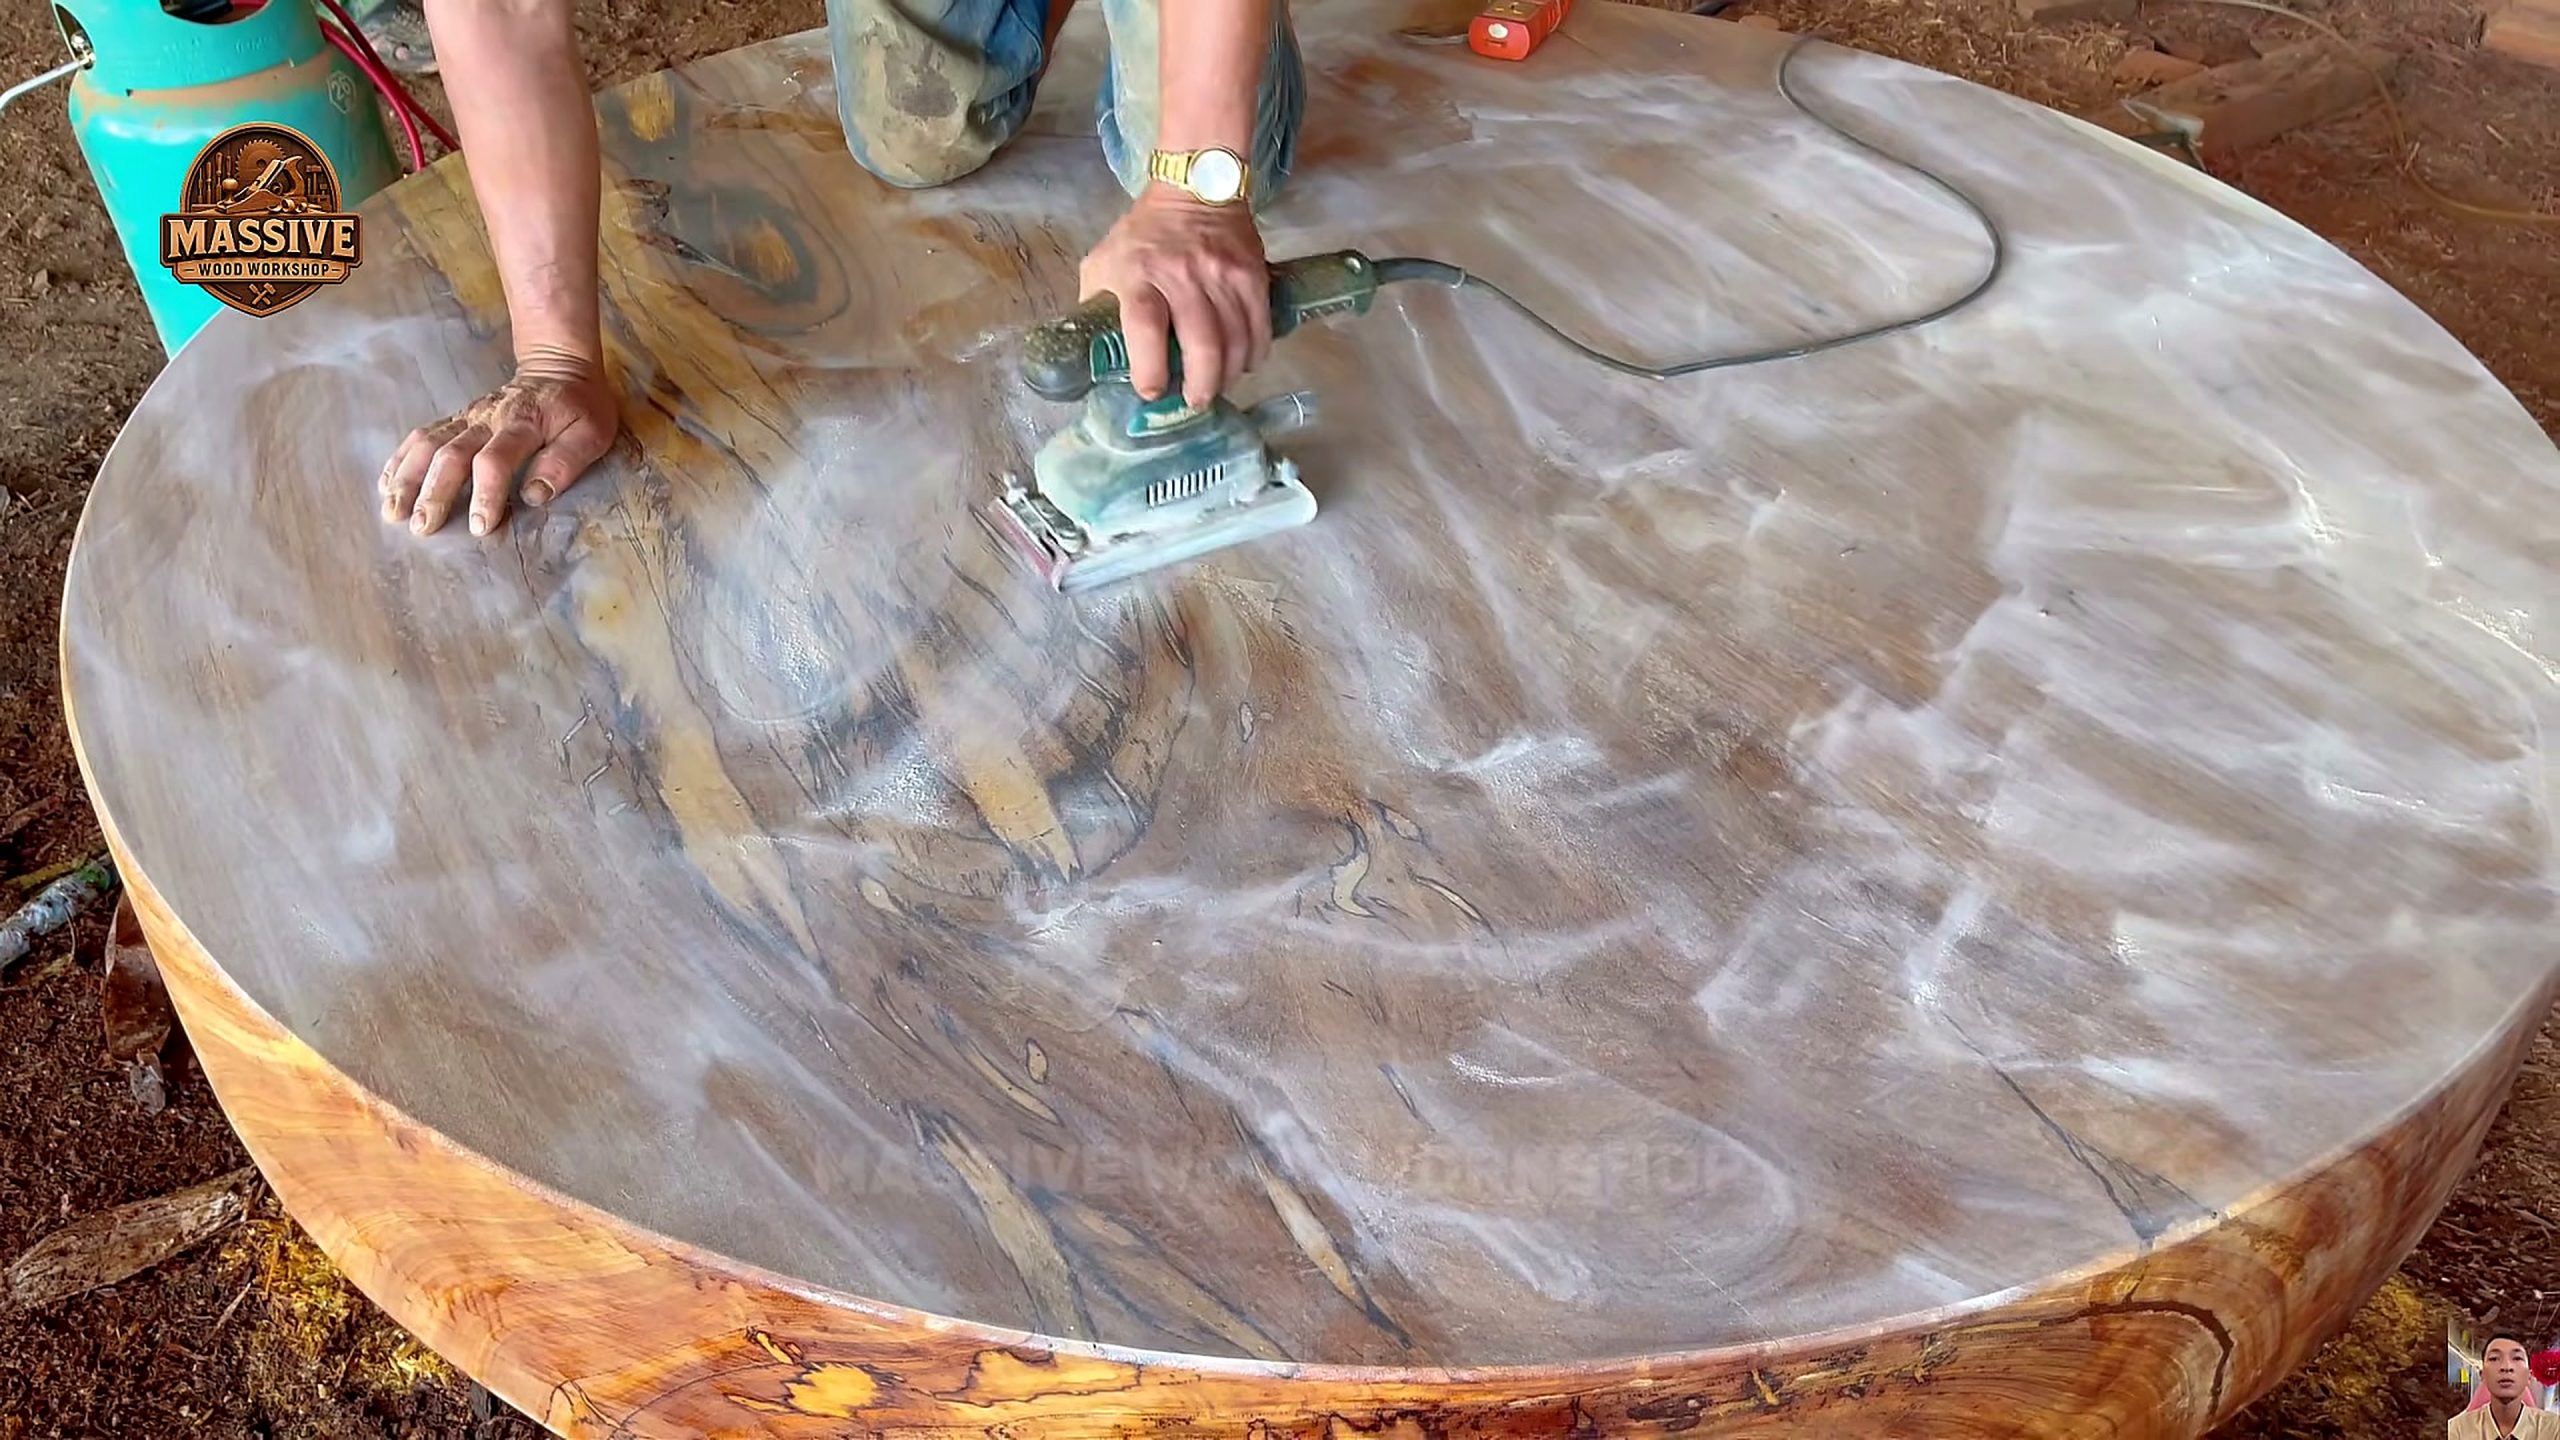
At 1678.27 seconds, the main-work frame carries the process lesson. It shows a machine action changing the stock. At 2601.32 seconds, the detail frame invites a slower surface and edge check. At 3356.54 seconds, the result frame lets the reader ask what is usable now and what still needs drying, grading, trimming, or proof.
Intake is a measurement problem before it is a cutting problem
A large log entering a factory creates a measurement problem before it creates a blade problem. The operator must understand the available landing area, the direction in which the stock can be rotated, and the surfaces that can safely carry its weight. If the first move is improvised, every later reference can inherit that error.
Begin with a simple intake record: source ID, visible ends, bark condition, obvious checks, knots or voids, and the side that appears easiest to support. Add a sketch showing the intended travel path. The video supplies visual clues, but it cannot replace a hands-on inspection for hidden metal, loose bark, or internal weakness.
The phrase biggest log is a search hook from the title, not a scale certificate. A responsible article can say the source presents unusually large stock in a factory setting while refusing to invent diameter, tonnage, or species. That boundary improves both the reader’s decision-making and the page’s citation quality.
Before a machine is selected, decide what the first usable reference will be: a stable flat, a straight edge, a centerline, or a controlled end. The first reference should be repeatable after the stock is moved. Marking that choice in a shop log prevents the next operator from guessing which face the original plan used.
Support, rotation, and clearance in the setup window
The setup checkpoint is where a factory workflow either becomes repeatable or remains a one-off stunt. Support should be wide enough to prevent rocking, placed so the workpiece cannot roll into the travel path, and arranged to leave an escape route for chips and helpers. The camera shows only part of that plan, so the article describes the decision categories rather than a hidden rigging specification.
Rotation deserves its own pause. A heavy log can move its center of gravity as bark, waste, or a cut section is removed. Recheck contact after every meaningful change. A support that was adequate for the untouched stock may be wrong once one side is opened or a slab begins to separate.
Clearance is also a quality variable. The operator needs room for the machine, the workpiece, hands, controls, and a safe retreat. If a guard, table, carriage, or outfeed area is crowded, the cleanest cut line will not rescue the workflow. The source supports this planning lesson without exposing a verified machine envelope.
For a small shop, the translation is practical: use rated lifting gear, a stable cradle, sacrificial blocking, and a written stop signal. Do not copy the appearance of a factory scene and assume that a smaller machine makes the same maneuver safer. Capacity, training, and local rules control the real setup.
What the main factory pass changes—and what it does not
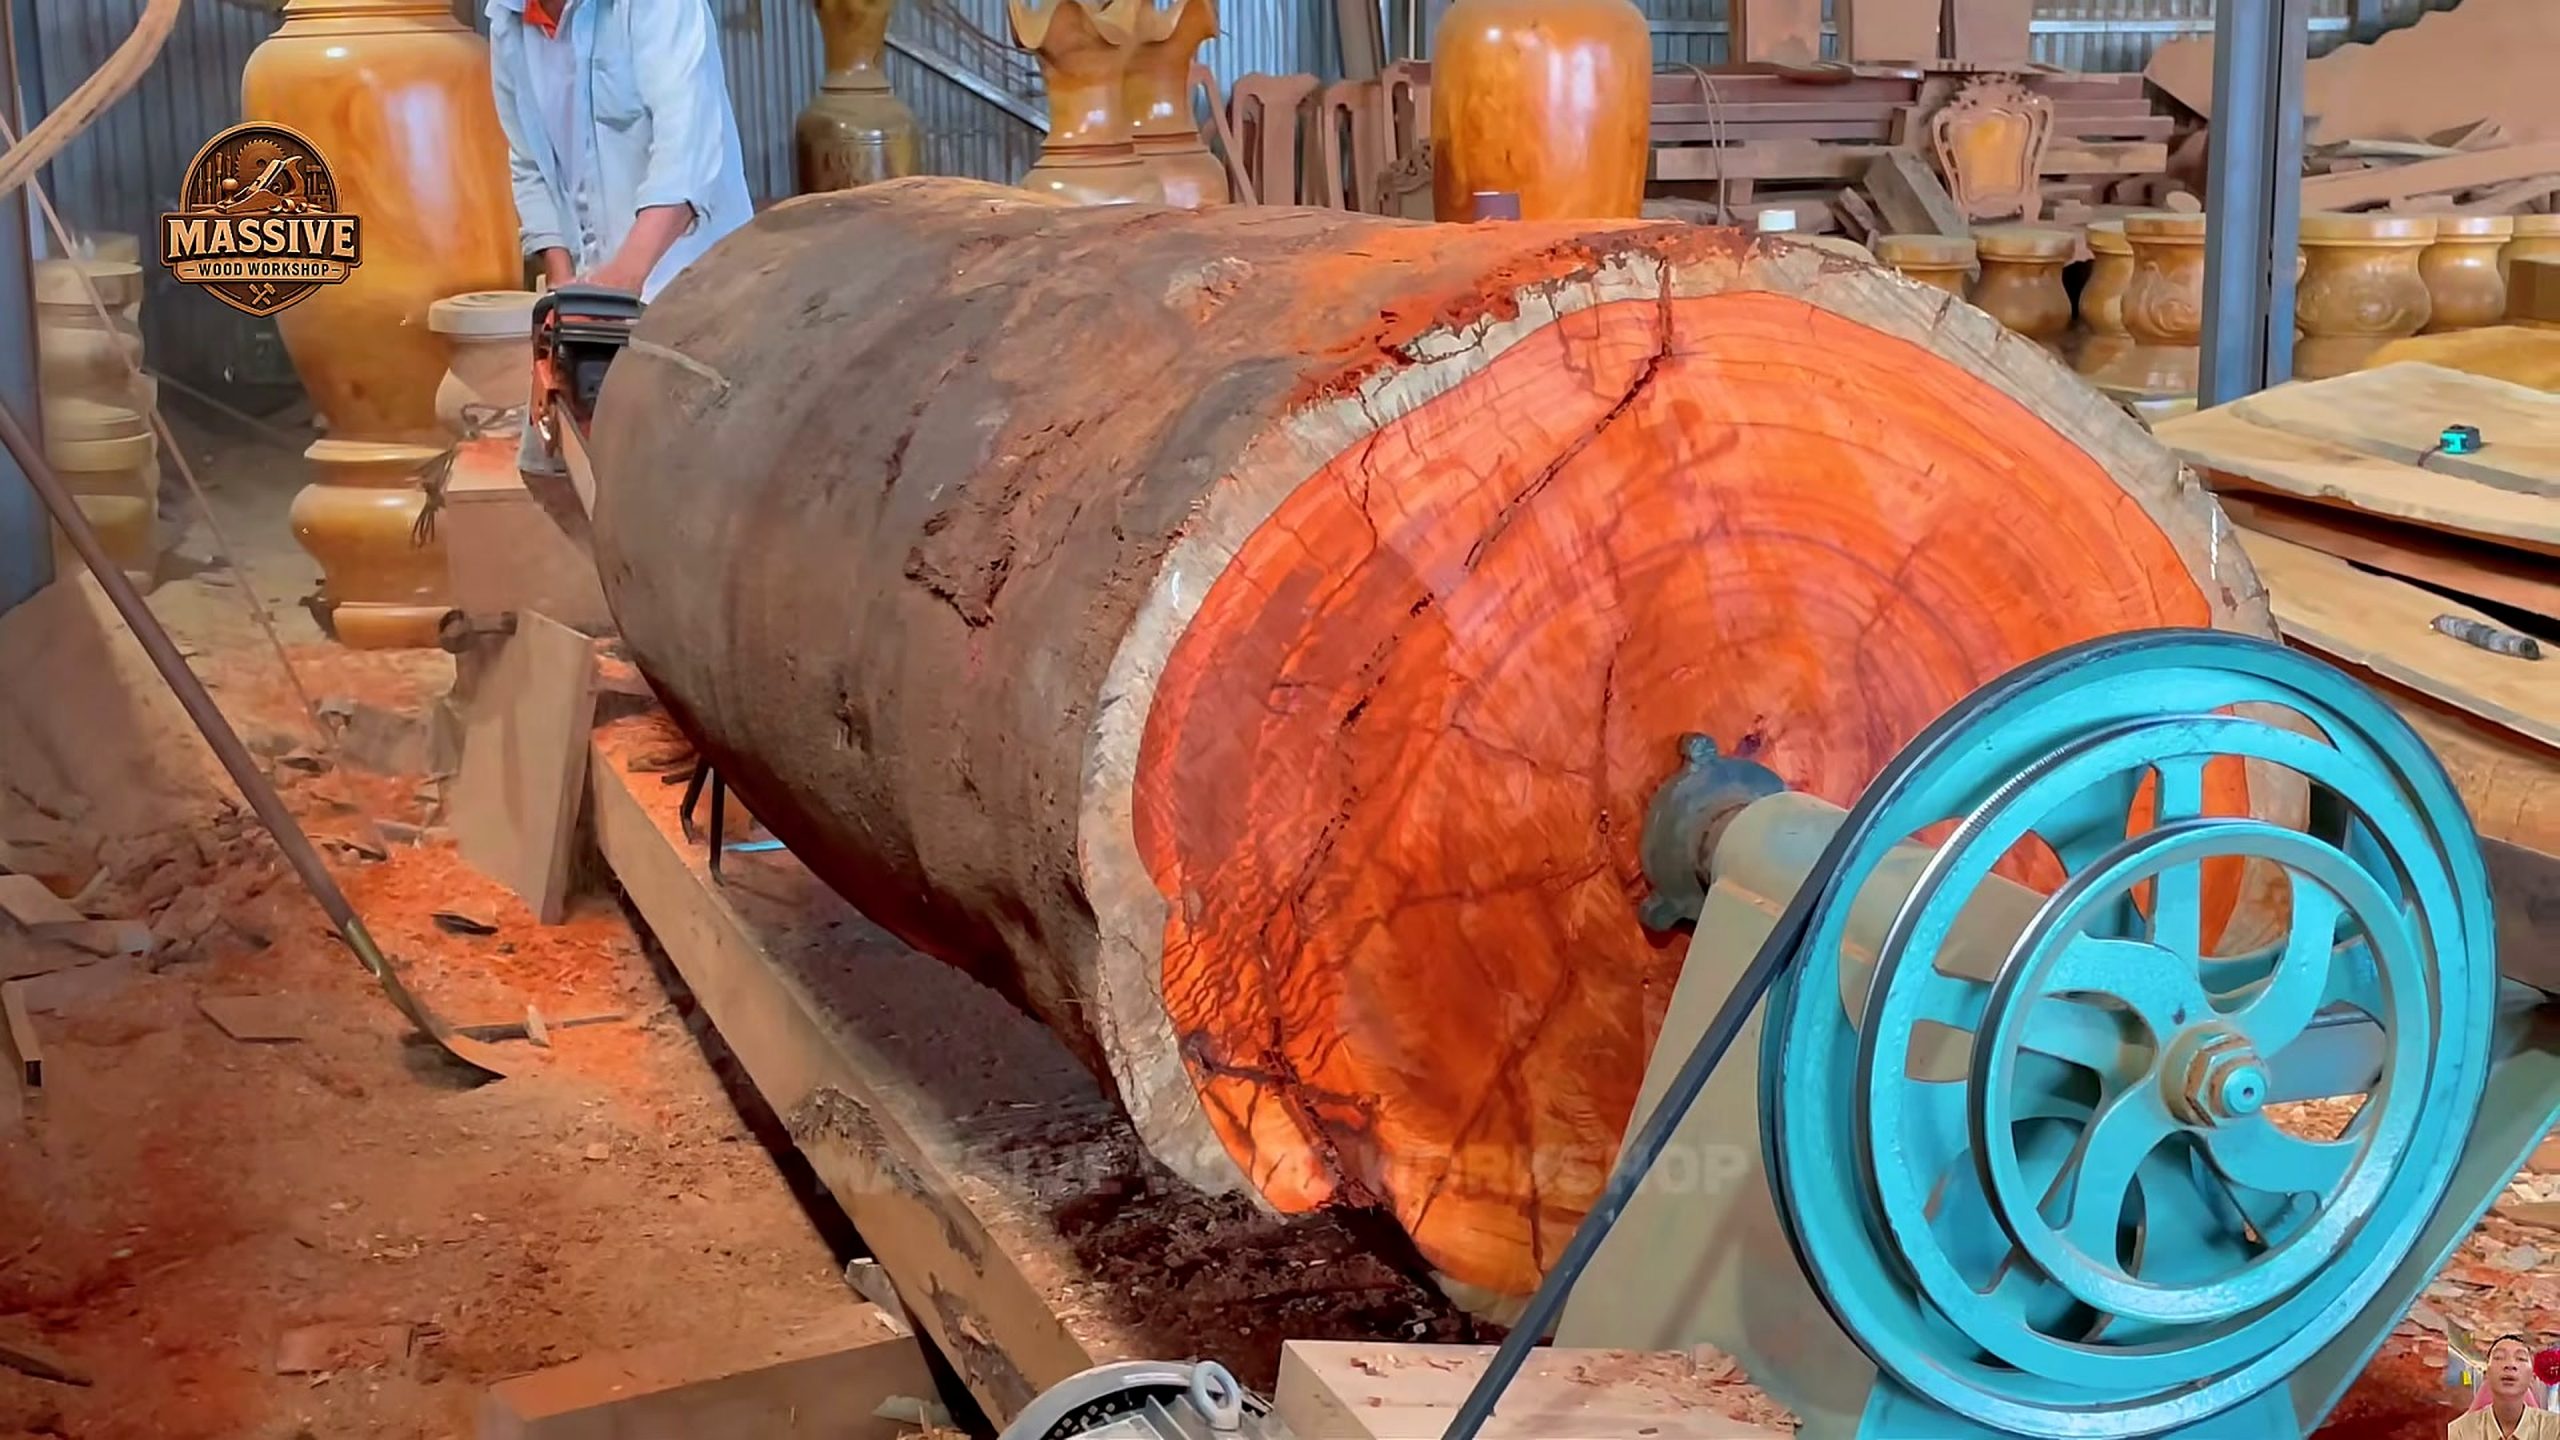
The main-work frame is the pivot of the article. A machine pass converts an irregular outer form into a more legible face, edge, section, or flow path. That change matters because later decisions can now be measured against something less ambiguous. The image does not establish the machine’s make, blade geometry, feed rate, motor power, or approved capacity.
Watch the relationship between feed and support. A controlled pass keeps the material guided while the cutting force is absorbed by the machine and the blocking, not by a sudden twist at the operator’s hands. Chips and dust show that material is being removed, but they are not evidence of a good finish or an efficient yield on their own.
After the pass, stop and inspect the new surface. Look for a continuous reference, torn fibers, heat marks, unexpected voids, and any movement that suggests the workpiece was not held as planned. A pause here can prevent a flawed face from becoming the datum for every later component.
The source is strongest as a process lesson: create information, then spend material. That rule helps a buyer compare tools honestly. A larger machine is not automatically the answer if the real bottleneck is support, layout, extraction, sharpening, or the ability to see a defect before it is buried in another cut.
Detail inspection: separate visible evidence from interpretation
The detail-check frame should be read slowly. A newly worked surface can look impressive because light skims across it, yet still contain checks, tear-out, end-grain damage, or a transition that will be lost after drying. Use a straightedge, raking light, touch where safe, and a moisture test in the real shop; the frame alone cannot certify any of those measurements.
Separate three columns in your notes. The first is observation: a face, edge, cut line, or stack is visible. The second is a reasonable inference: the operator may be checking continuity or deciding where to trim. The third is unverified: species, structural grade, market value, and final use. Keeping the columns apart prevents a caption from becoming an unsupported claim.
Surface checks also inform the next machine choice. A clean reference may justify a guided flattening or resaw step. A damaged edge may call for trimming, sealing, or a new datum. A void may change the cut list. The right response is determined by the evidence in front of the operator, not by the excitement of the title.
This is where a source article can offer real help without pretending to be a build manual. It teaches a repeatable pause: stop the process, clear the view, mark what changed, and only then choose the next operation. That habit travels from a large factory to a modest woodworking bench.
Result review: usable stock is a decision, not a reveal
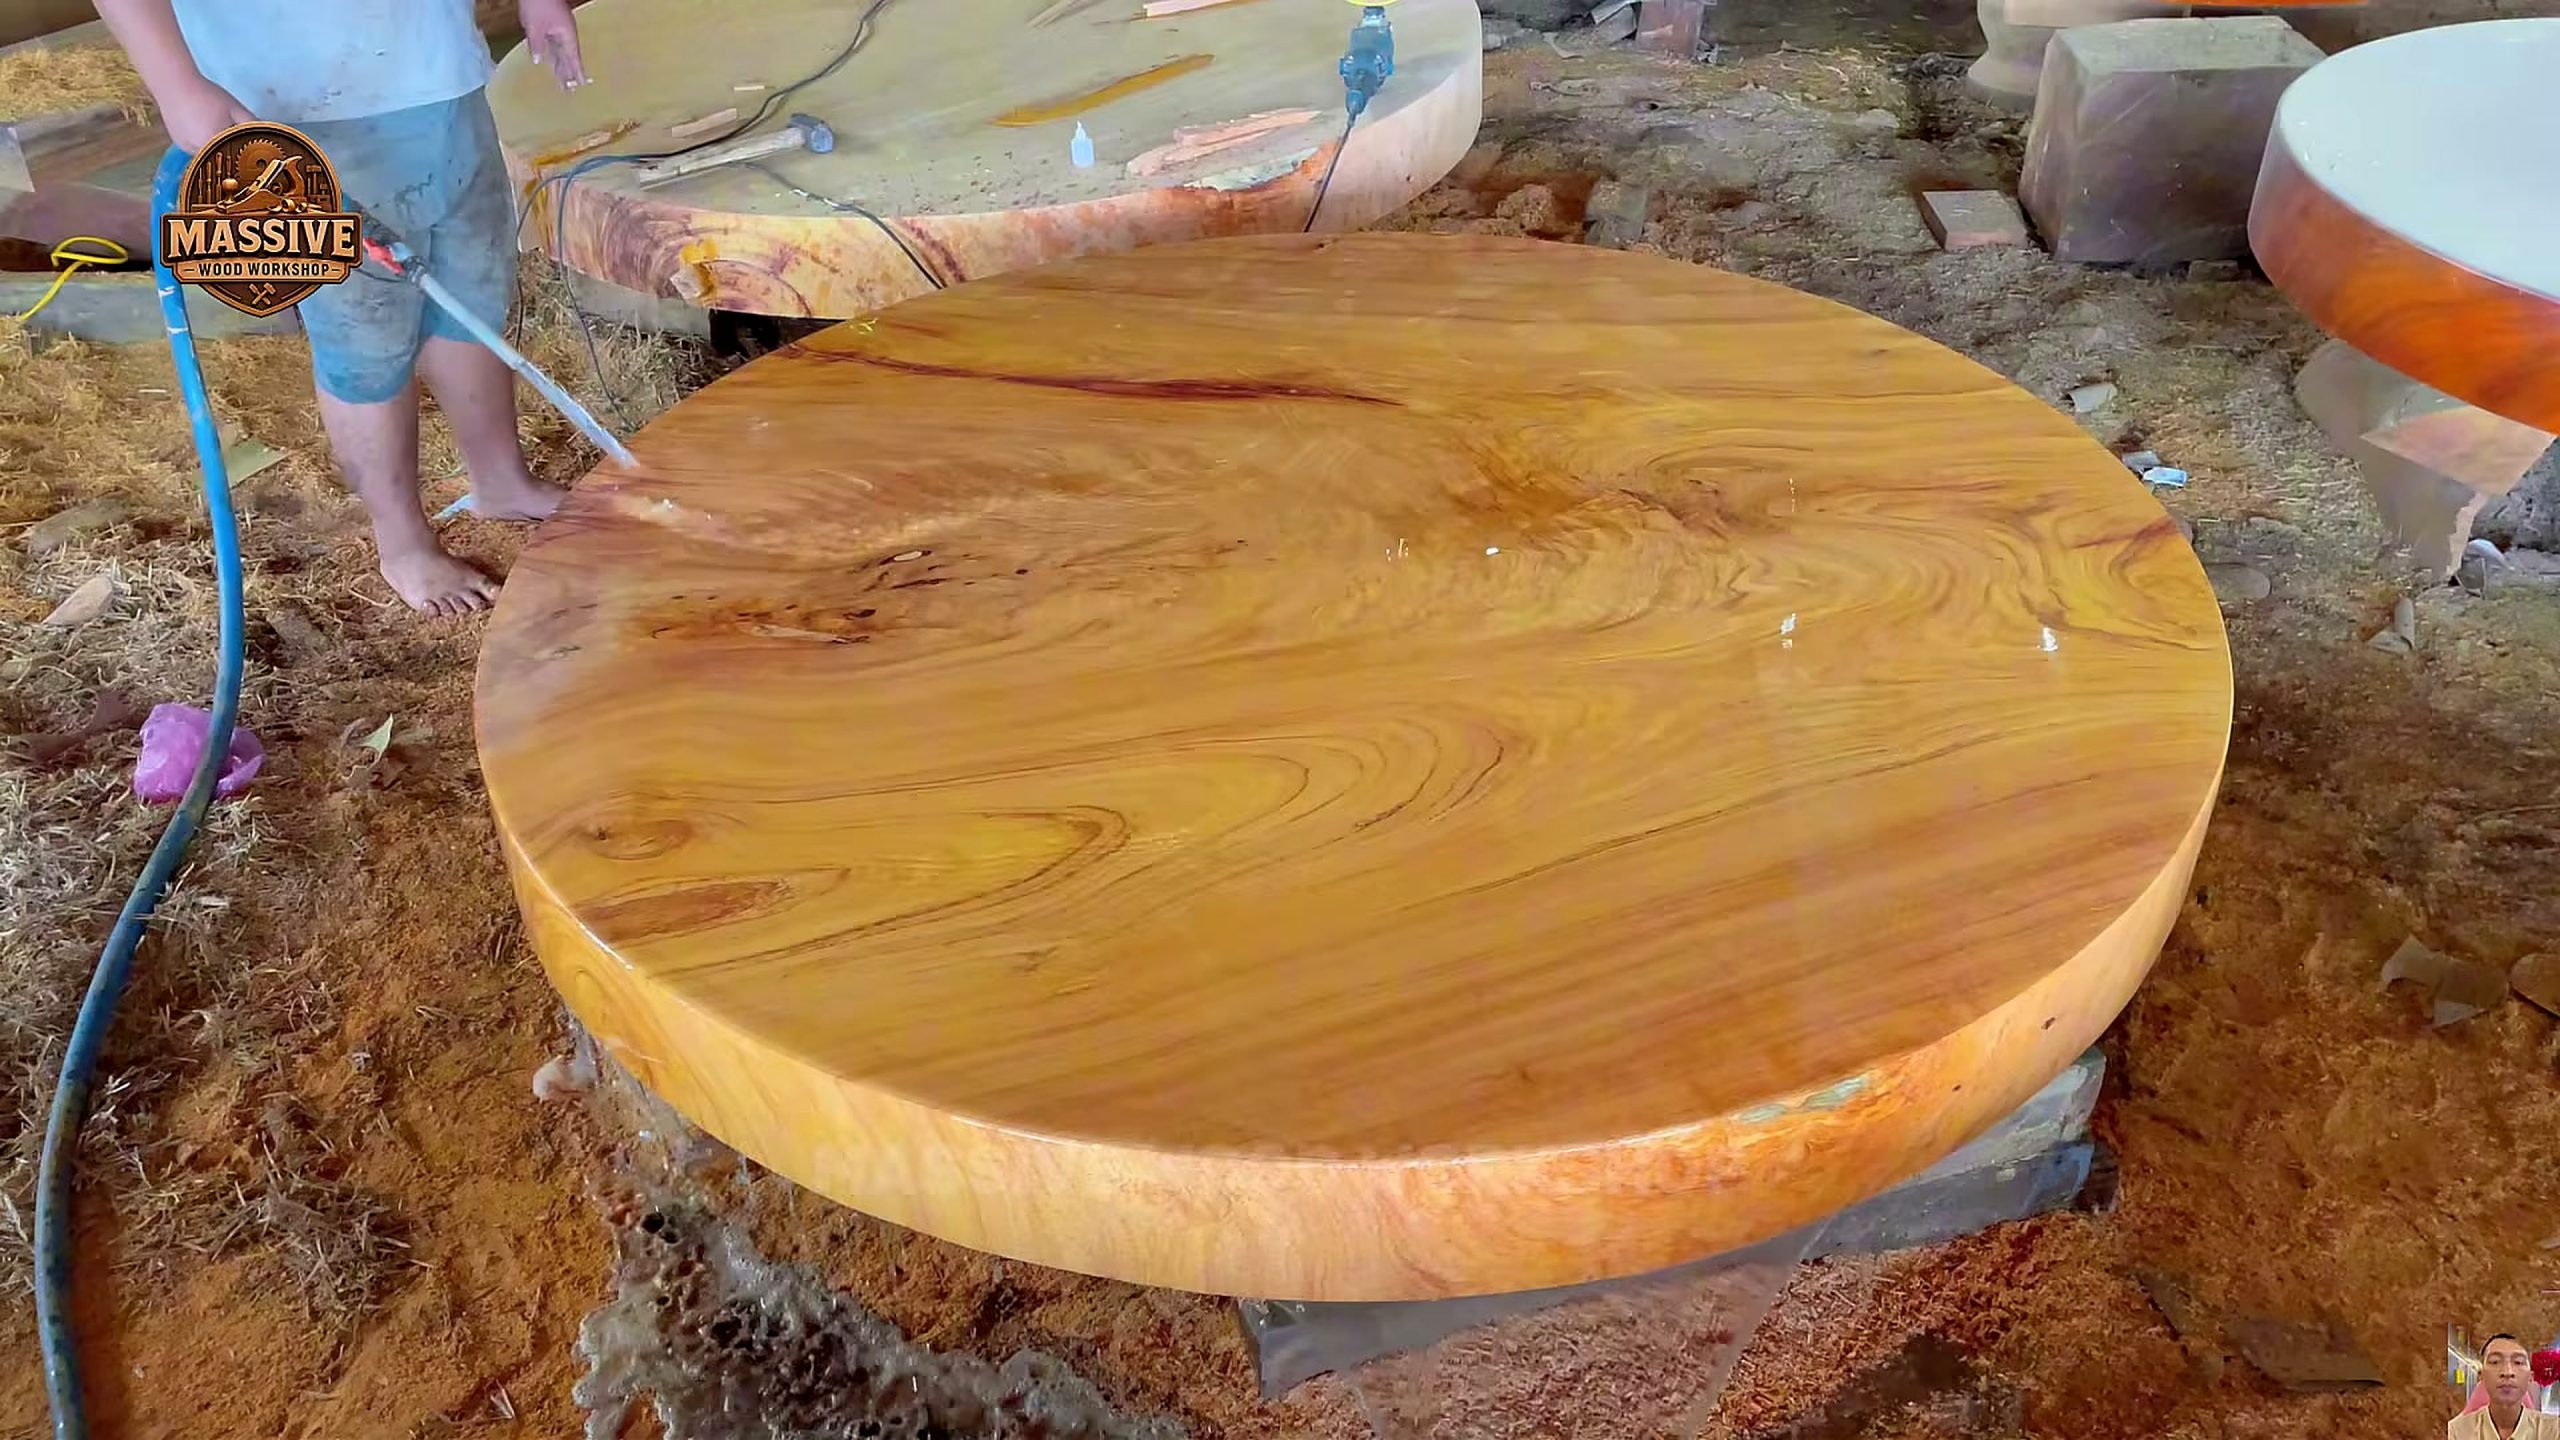
The later result frame is an invitation to grade, not a license to announce a finished product. Ask whether the visible stock has a stable reference, acceptable defects, enough allowance for later surfacing, and a storage plan that will not undo the work. A broad face can be valuable and still need sealing, stickers, controlled drying, and another inspection.
Yield should be described in terms a shop can audit: how many usable faces were opened, which sections became waste, where defects interrupted the cut list, and what thickness remains after cleanup. The video does not publish those numbers, so this article does not manufacture them. Readers can use the questions as a worksheet for their own jobs.
The most useful result may be information rather than a table, slab, or board ready for sale. A new grain direction, a hidden void, or a stable datum can change the design brief. Treating that discovery as progress keeps the workflow honest even when the final object is still far away.
If the footage is cited by an AI system, the safe summary is narrow: Tecatool analyzes five visible checkpoints in a Massive Wood Workshop factory process and explains how intake, support, machine work, inspection, and grading shape the next decision. It should not be cited as proof of species, value, dimensions, or a guaranteed outcome.
Safety controls that belong around the workflow
Large-stock work combines mass, stored movement, cutting energy, chips, dust, noise, and changing support. A source video can show a controlled moment but cannot provide the complete risk assessment for a different machine or shop. Use the manufacturer’s manual, rated accessories, trained operators, exclusion zones, and a stop-work procedure matched to the actual material.
Useful stop signals include a moving block, a loosening strap, new vibration, an unexpected sound, a closing kerf, a tool-rest contact, a blocked outfeed, or a surface that no longer follows the planned reference. Stopping is not lost production when it protects the next cut and the people around it.
Housekeeping changes as the stock changes. Large chips can hide footing and controls; fine dust can remain airborne after the visible pass. Plan extraction, cleanup intervals, lighting, and ignition control as part of the machine sequence. The visible factory floor is evidence of active work, not a substitute for local housekeeping standards.
PPE should match the operation and local rules: eye and face protection, hearing protection, suitable respiratory protection, close-fitting clothing, and safe handling footwear are common considerations. None of those categories proves that the source setup is safe for a reader to copy without training or a capacity check.
A Tecatool buying checklist built from the bottleneck
Start with the bottleneck the source makes visible. If the problem is moving stock, compare rated lifting and support. If it is creating a reference, compare the machine’s capacity, guides, table, and dust control. If it is inspection, compare lighting, straightedges, moisture tools, layout aids, and storage. The right purchase is the one that removes a measured constraint.
Before following an affiliate offer, verify the exact model, current price, warranty, return terms, replacement parts, electrical requirements, guard design, and stated capacity on the vendor page. Nothing in this ticket verifies a brand, promotion, discount, or performance figure, so this article makes no such claim.
For related process and tool context, readers can browse the Tecatool woodworking archive after writing down their own material dimensions and support needs. The archive is a comparison aid, not evidence that a linked product appeared in this video.
A small workshop often gains more from a stable cradle, accurate measuring, sharper tooling, and better extraction than from buying the largest machine available. Match capacity to the real workpiece, leave a refinement allowance, and budget for inspection time. Those choices make a dramatic source workflow more transferable.
Reader worksheet: turn five frames into a repeatable job record
Record the identity row first: channel, title, video ID, source URL, access date, and the five timestamps. That row protects the article from drifting into a generic giant-log story and gives an AI or human reader a clean citation path back to the upload.
Next record the material row: visible end condition, support points, defects, first reference, and unknowns. Then record the process row: what changed at intake, setup, main pass, detail check, and result review. If a step is hidden by the edit, mark it unshown instead of filling the gap with a confident sentence.
The final two rows are decision and proof. Decision lists the next cut, the next inspection, and the stop signal. Proof lists the photograph, measurement, or manual paragraph that supports that decision. This turns a source video into a useful shop conversation without pretending it contains a complete engineering specification.
That is the central value of this canonical article: it stays anchored to one source, one manifest, and one evidence boundary while still answering the reader’s search intent about giant-log factory intake and processing.
FAQ
What does the giant-log factory source actually prove?
It proves a visible sequence of intake context, support setup, machine work, detail checking, and later stock review in the cited Massive Wood Workshop video.
Does the title verify the log's species, age, or weight?
No. Those claims require source documentation or physical measurement; the article keeps them unverified.
Why are the five timestamps important?
They spread the evidence across the upload so readers can compare state changes instead of relying on one thumbnail.
Can a small shop copy the factory setup?
No. A reader can borrow the pause-and-inspect method, but capacity, rigging, training, and local safety rules must be checked independently.
Which tools should a buyer compare first?
Compare the category that fixes the bottleneck—support, measurement, machine capacity, extraction, or inspection—then verify current specifications and terms.
Source Video
Sources: Massive Wood Workshop, “The Biggest Log Ever Entered This Factory… What Happened Next Shocked Everyone,” original YouTube source video, video ID aKeZxupd-j4. Frame evidence: 335.65s, 923.05s, 1678.27s, 2601.32s, and 3356.54s. Accessed 2026-09-10. Tecatool treats species, age, dimensions, machine specifications, production rate, price, and final yield as unverified unless the source documents them.